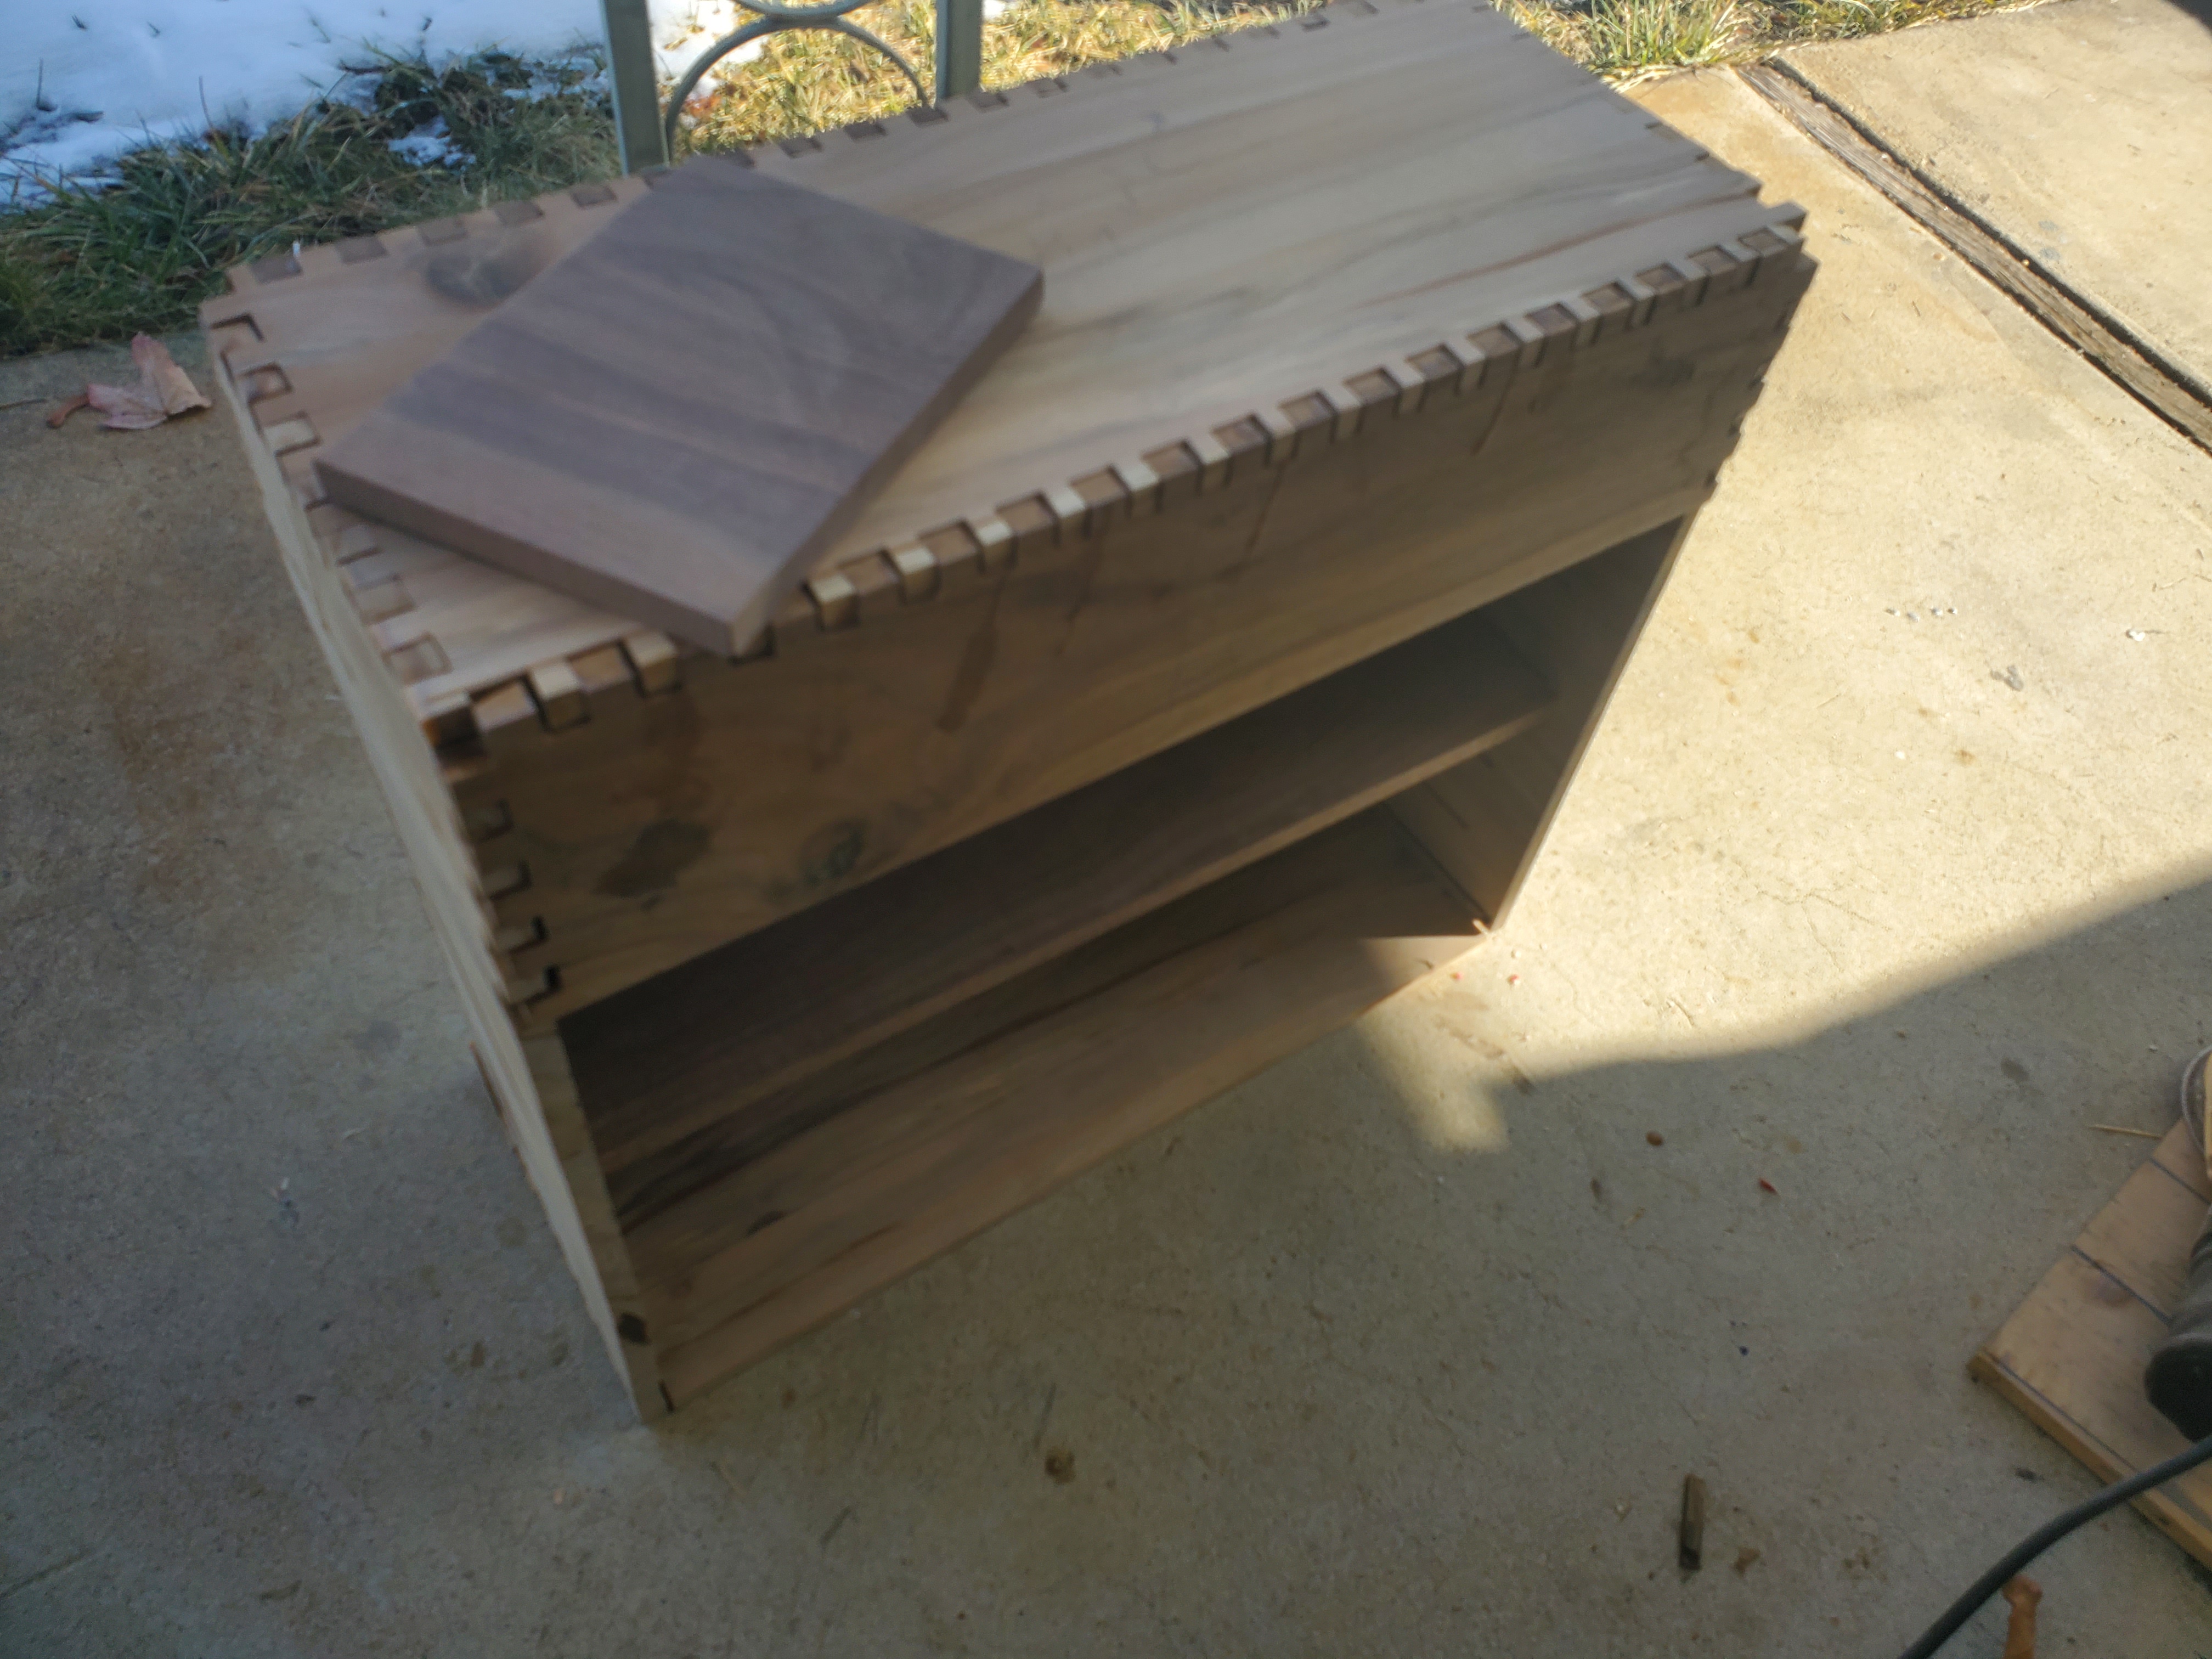
Showing posts with label toolbox. Show all posts

Friday, November 17, 2023

Puffed Out Chest - Part B

I started a machinists tool chest build. Part A was over at  http://www.silverhawk.net/2022/12/puffed-out-chest-part-a.html .  Anyway, moving on to the next task of filling the box joint imperfection with epoxy to strengthen and make it a more interesting build.

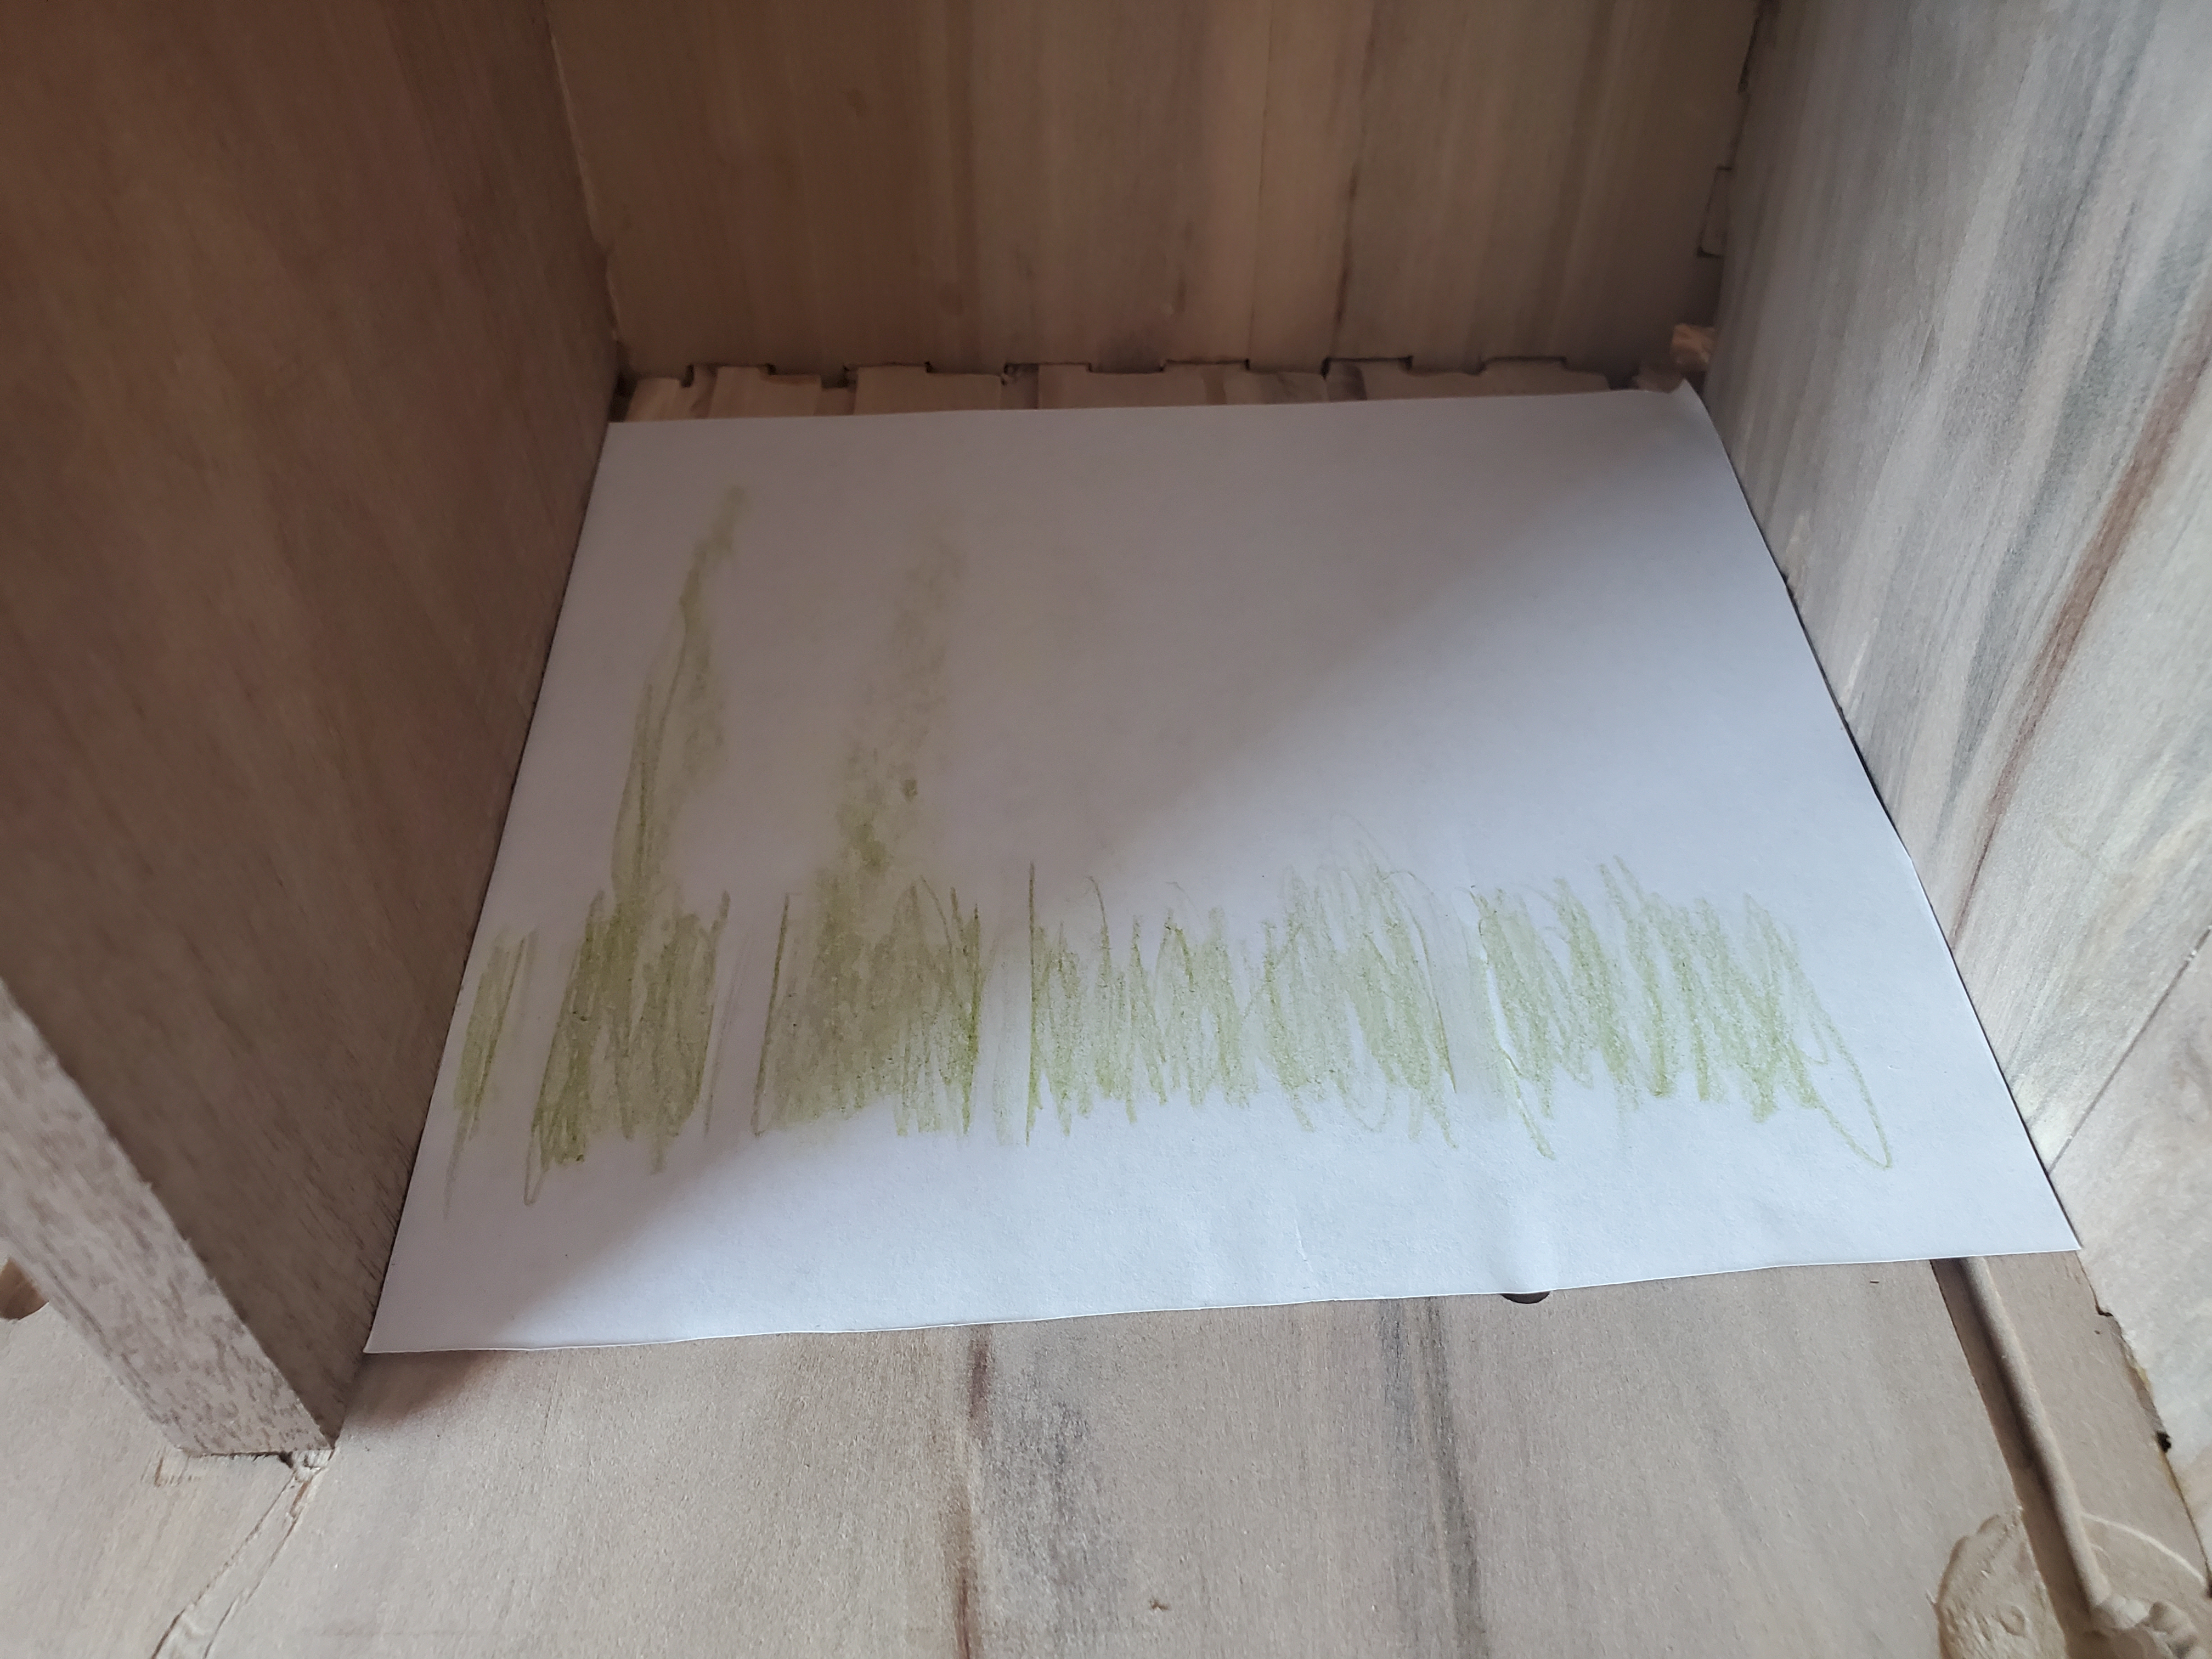
Before I get there, I need to have the internal vertical boards completed.  Transferring the outside slots to the inside slots was something I put off as long as possible because I didn't know how. I had an epiphany one night about how.  I grabbed some paper from the printer, scissors, and a crayon.  I trimmed a piece of paper to fit perfectly in the space that the boards would fit, labelled the paper with where edges were, and then used the crayon to mark the grooves on the paper.


At first, I tried fancy ways of using the paper on the board (cutting out grooves, etc), because the markings on top need to go face down on the other board, or we'd end up with a mirrored board.  I tried folding and cutting the slots with the scissors.


But ultimately, I found it easier to simply fold along the markings, then use a pencil to mark the board, and a straight edge to complete the lines.

The next phase was to drill the panel latching hardware.  Starting with the front panel pins, I needed a vertical (parallel) hole.  Worried about how to do this, I settled on using a square to hold it perpendicular to the drill press table.

While I could install the two internal panels, I thought it would be the perfect time to fill the cracks in the box joints and seal the boxes up.  I dutifully taped everything up, and kept worrying about filling those gaps cut in for the drawer slides.  It took me a night thinking things through before I realized I could lay the box on it's back, open the side seals in order to pour epoxy into those gaps, and let them fill the cracks.  It would allow me to fill up to the back of the boxes and not fill in any of the drawer slide groves.


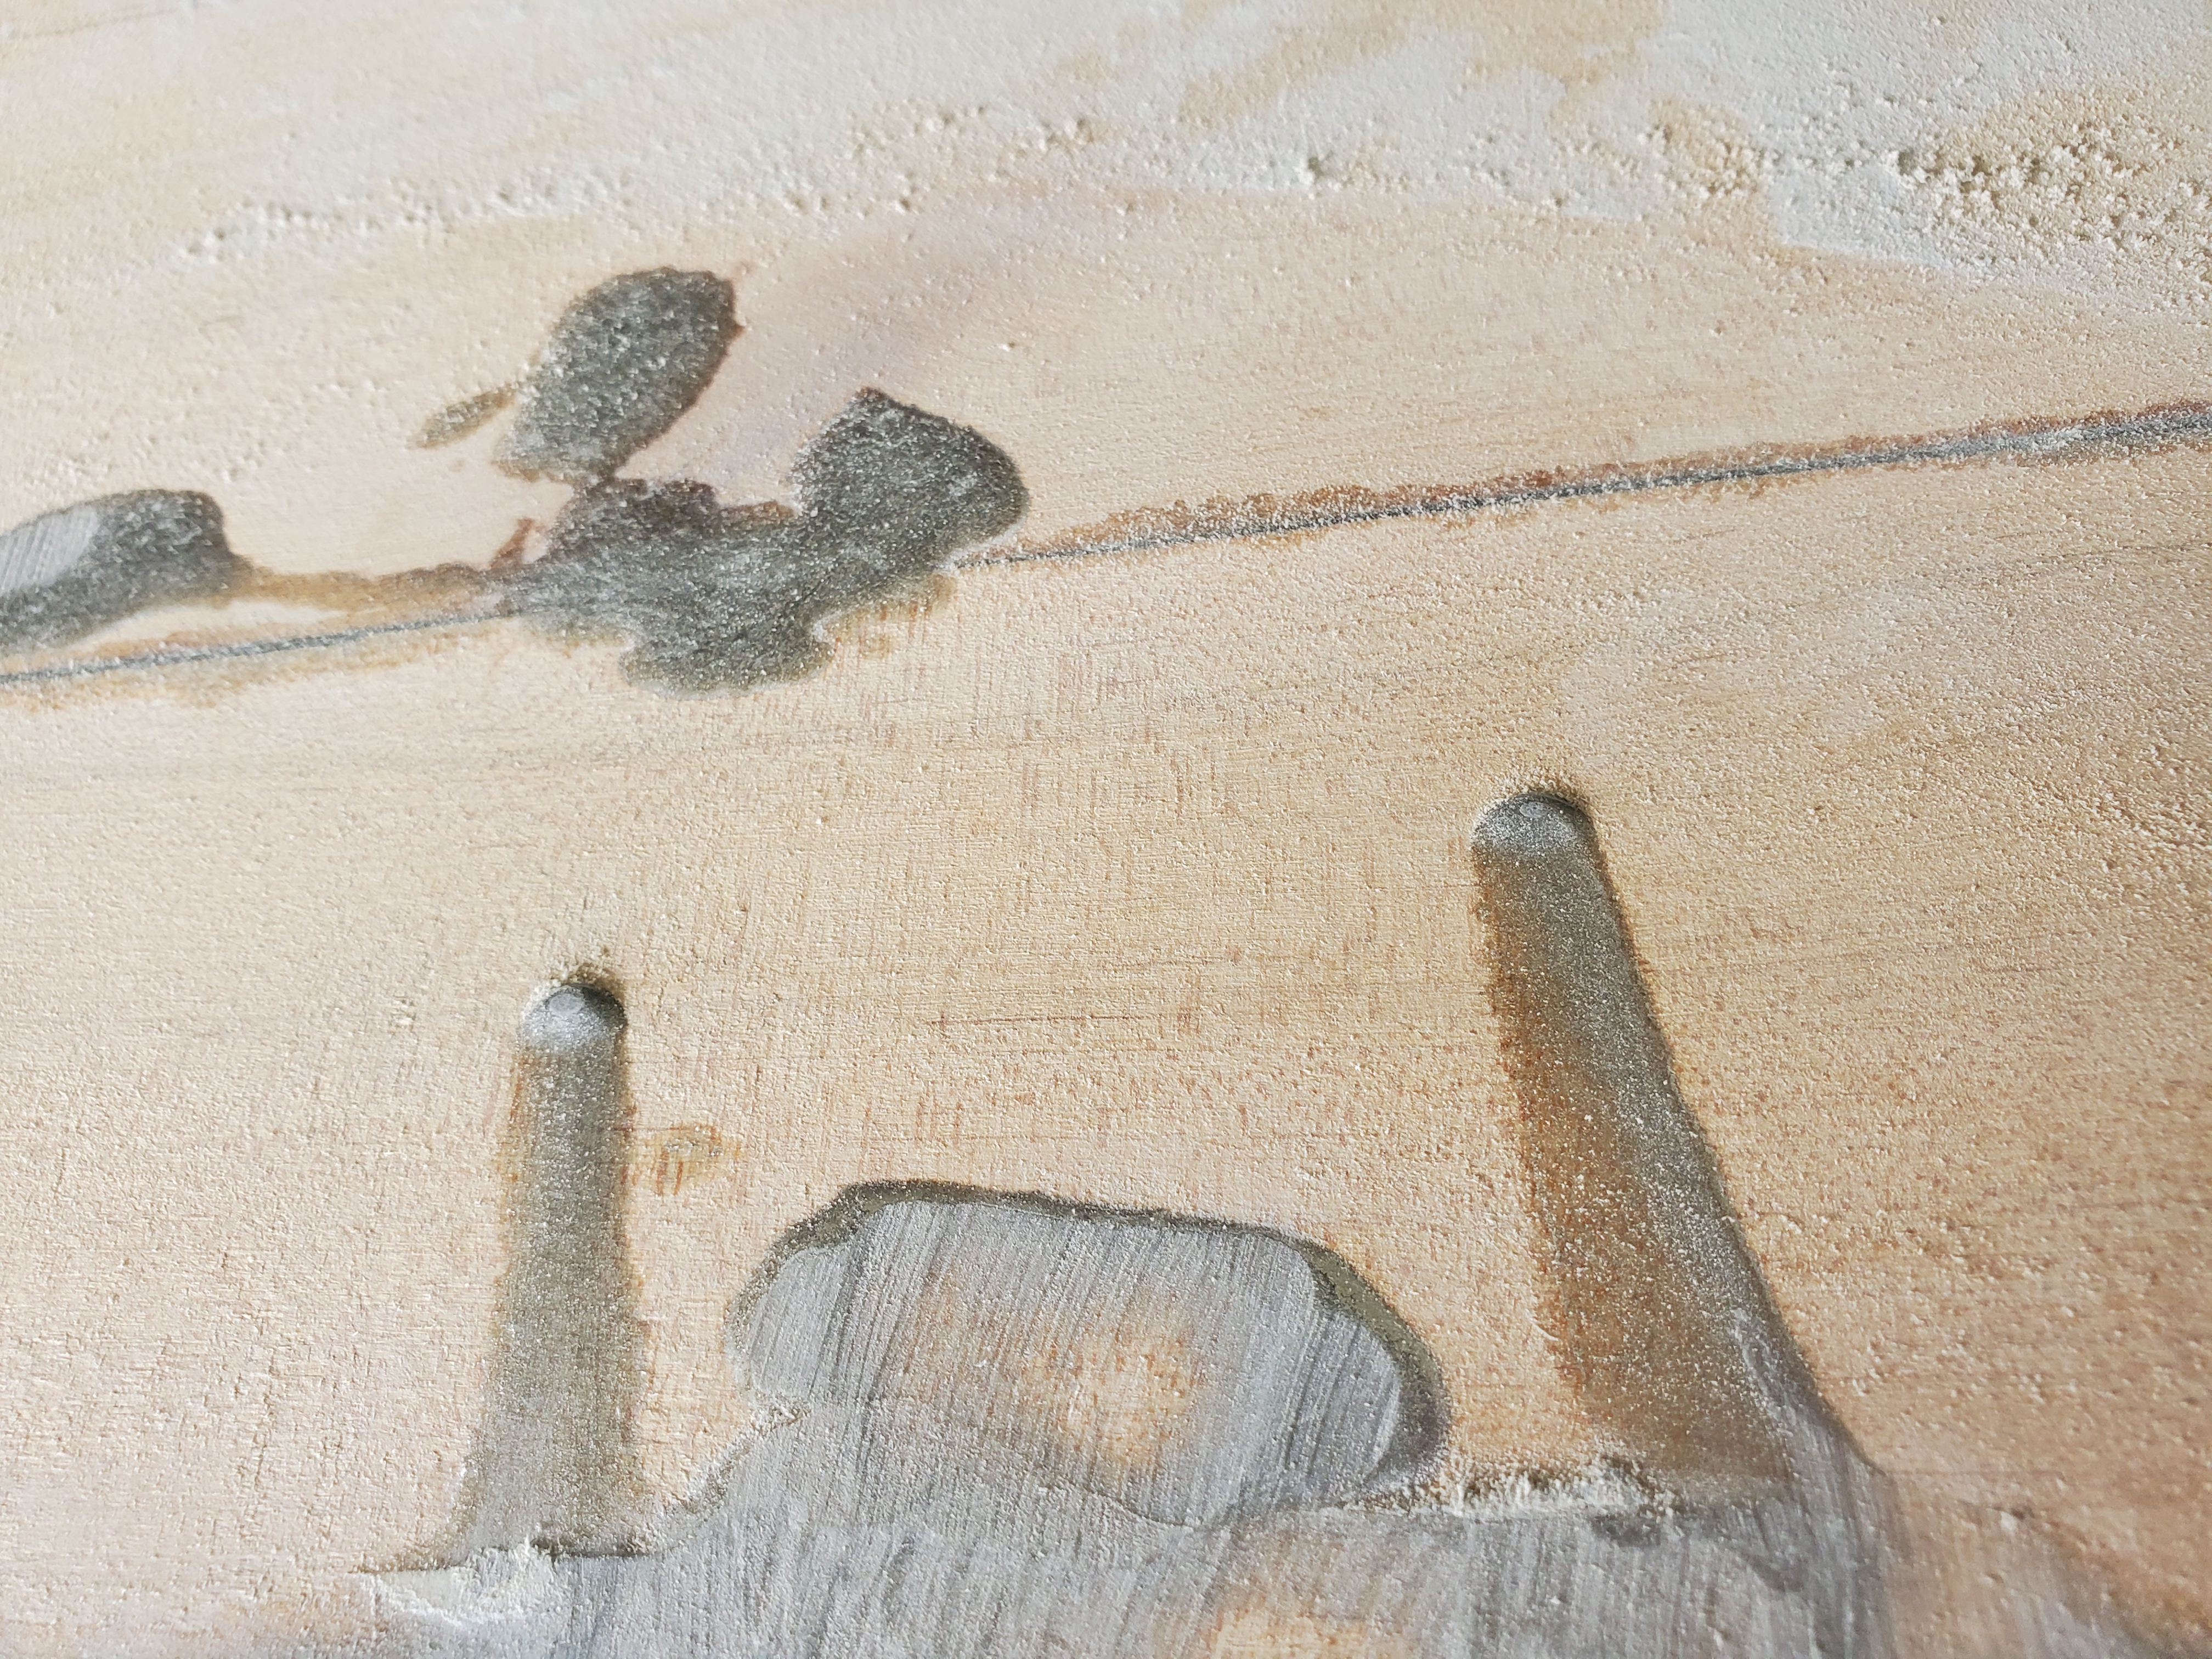
I needed to take my time on this.  Filling from the sides and letting it nearly set up would allow me to pour another little bit and get things to seal up faster as things cured.  (This was the perfect time to fill the laser-engraving on the front door to match - I did a little mica powder, and a lot of clear, so it could have an interesting effect.)

There was a lot of interrupted epoxy pours. I was using a "deep pour" epoxy made to work with thicker things such as lathe blanks, river tables, and similar things where you need a lot of thickness.  This wasn't because of thickness, but simply because this is both "thin" (e.g. it is very viscous and liquid and can fill cracks easily) as well as long curing.  That alone should allow me to fill all the voids, but it does take a great deal of time to build a suitable base and sealed edges.

Two boxes have have the majority of the voids and cracks filled at this point, so I let them sit for a day or two.  Once I was absolutely sure the epoxy had cured, it was time to sand it back down to flush with the wood surfaces again.

The logos in the front doors came out fantastic, though the silver is a little dark.  I'm not sure what will be needed there.  The gold turned out to be two separate hues of gold - one a little more orange gold (or "antique"), the other being a bright "queens" gold.


There were some areas where I had quite the overfill, because I'd rather make sure we got it everywhere.  I used the tablesaw to trim that off, a grinder to remove large volumes quickly, and then the sander to get it back to where it should be.

The inside was the most painful - I needed a small sander with a corner.  I used a Black and Decker "mouse", and that seemed to let me get into the cracks.  These little sanders come to a point on the tip, allowing you to get into the corners.

Once that was complete, I had to cut 66 small "boards" that were 0.232" thick (to fit into the grooves), 0.263" tall (to protrude as drawer slides), and 6" long (one chest, my "scrap" one, had only 4.875" of space for them, since it was adjusted later because I scrapped a board).  There are three tool chests, each with 11 drawers (that makes 33), and since these require one on each side, 33 gets doubled.  That was fun.  All of those were then glued into place.


Once dried, the inner vertical boards will need to be sanded and have my crooked lines filled with epoxy to match the carcasses, then I can perform the final fitment and glue those in.

Before I do that, though, I have to drill the holes to house the front panel locking pins.  As I write this, there are a multitude of ways to accomplish a long, parallel hole.  Keep in mind that I didn't think of a better way until I was through two of the three chests, so here we go.

First, I have a drill press table that was trammed in to within 0.002" over 16", so I knew I had accuracy for that one.  I took this to the drill press to bore the face lengthwise the pins.  Here's hoping I'm right and that this works.

This was one operation that took time.  First, if I had any angle instead of parallelism on that front facing bin panel, I'd likely pop out the back.  Second, the drill bit was a longer one (12" long) on a 1/4" bore to fit the springs and pins.  This had to be as perfect as I can, and ended up being the longest set up operation I've ever done.  It took me an hour for each hole (two for each tool chest).  But, I can rest assured that I am as good as I can be.

One additional gotcha was my drill press only has 3" of range, and these panels are anywhere from 3" to 4" (not all tool chests are exactly the same size).  So, I had to drill this in stages.  Painful, really, but I made it.

If you are using the Gerstner pin hardware, the entire bore has to be 1/4" in diameter to house the spring, and the ends are 0.3125" (5/16") for the caps, at least 0.260" deep.  So, drill out with the long 1/4" bit was the first step.

Drilling had to be in stages, of course.
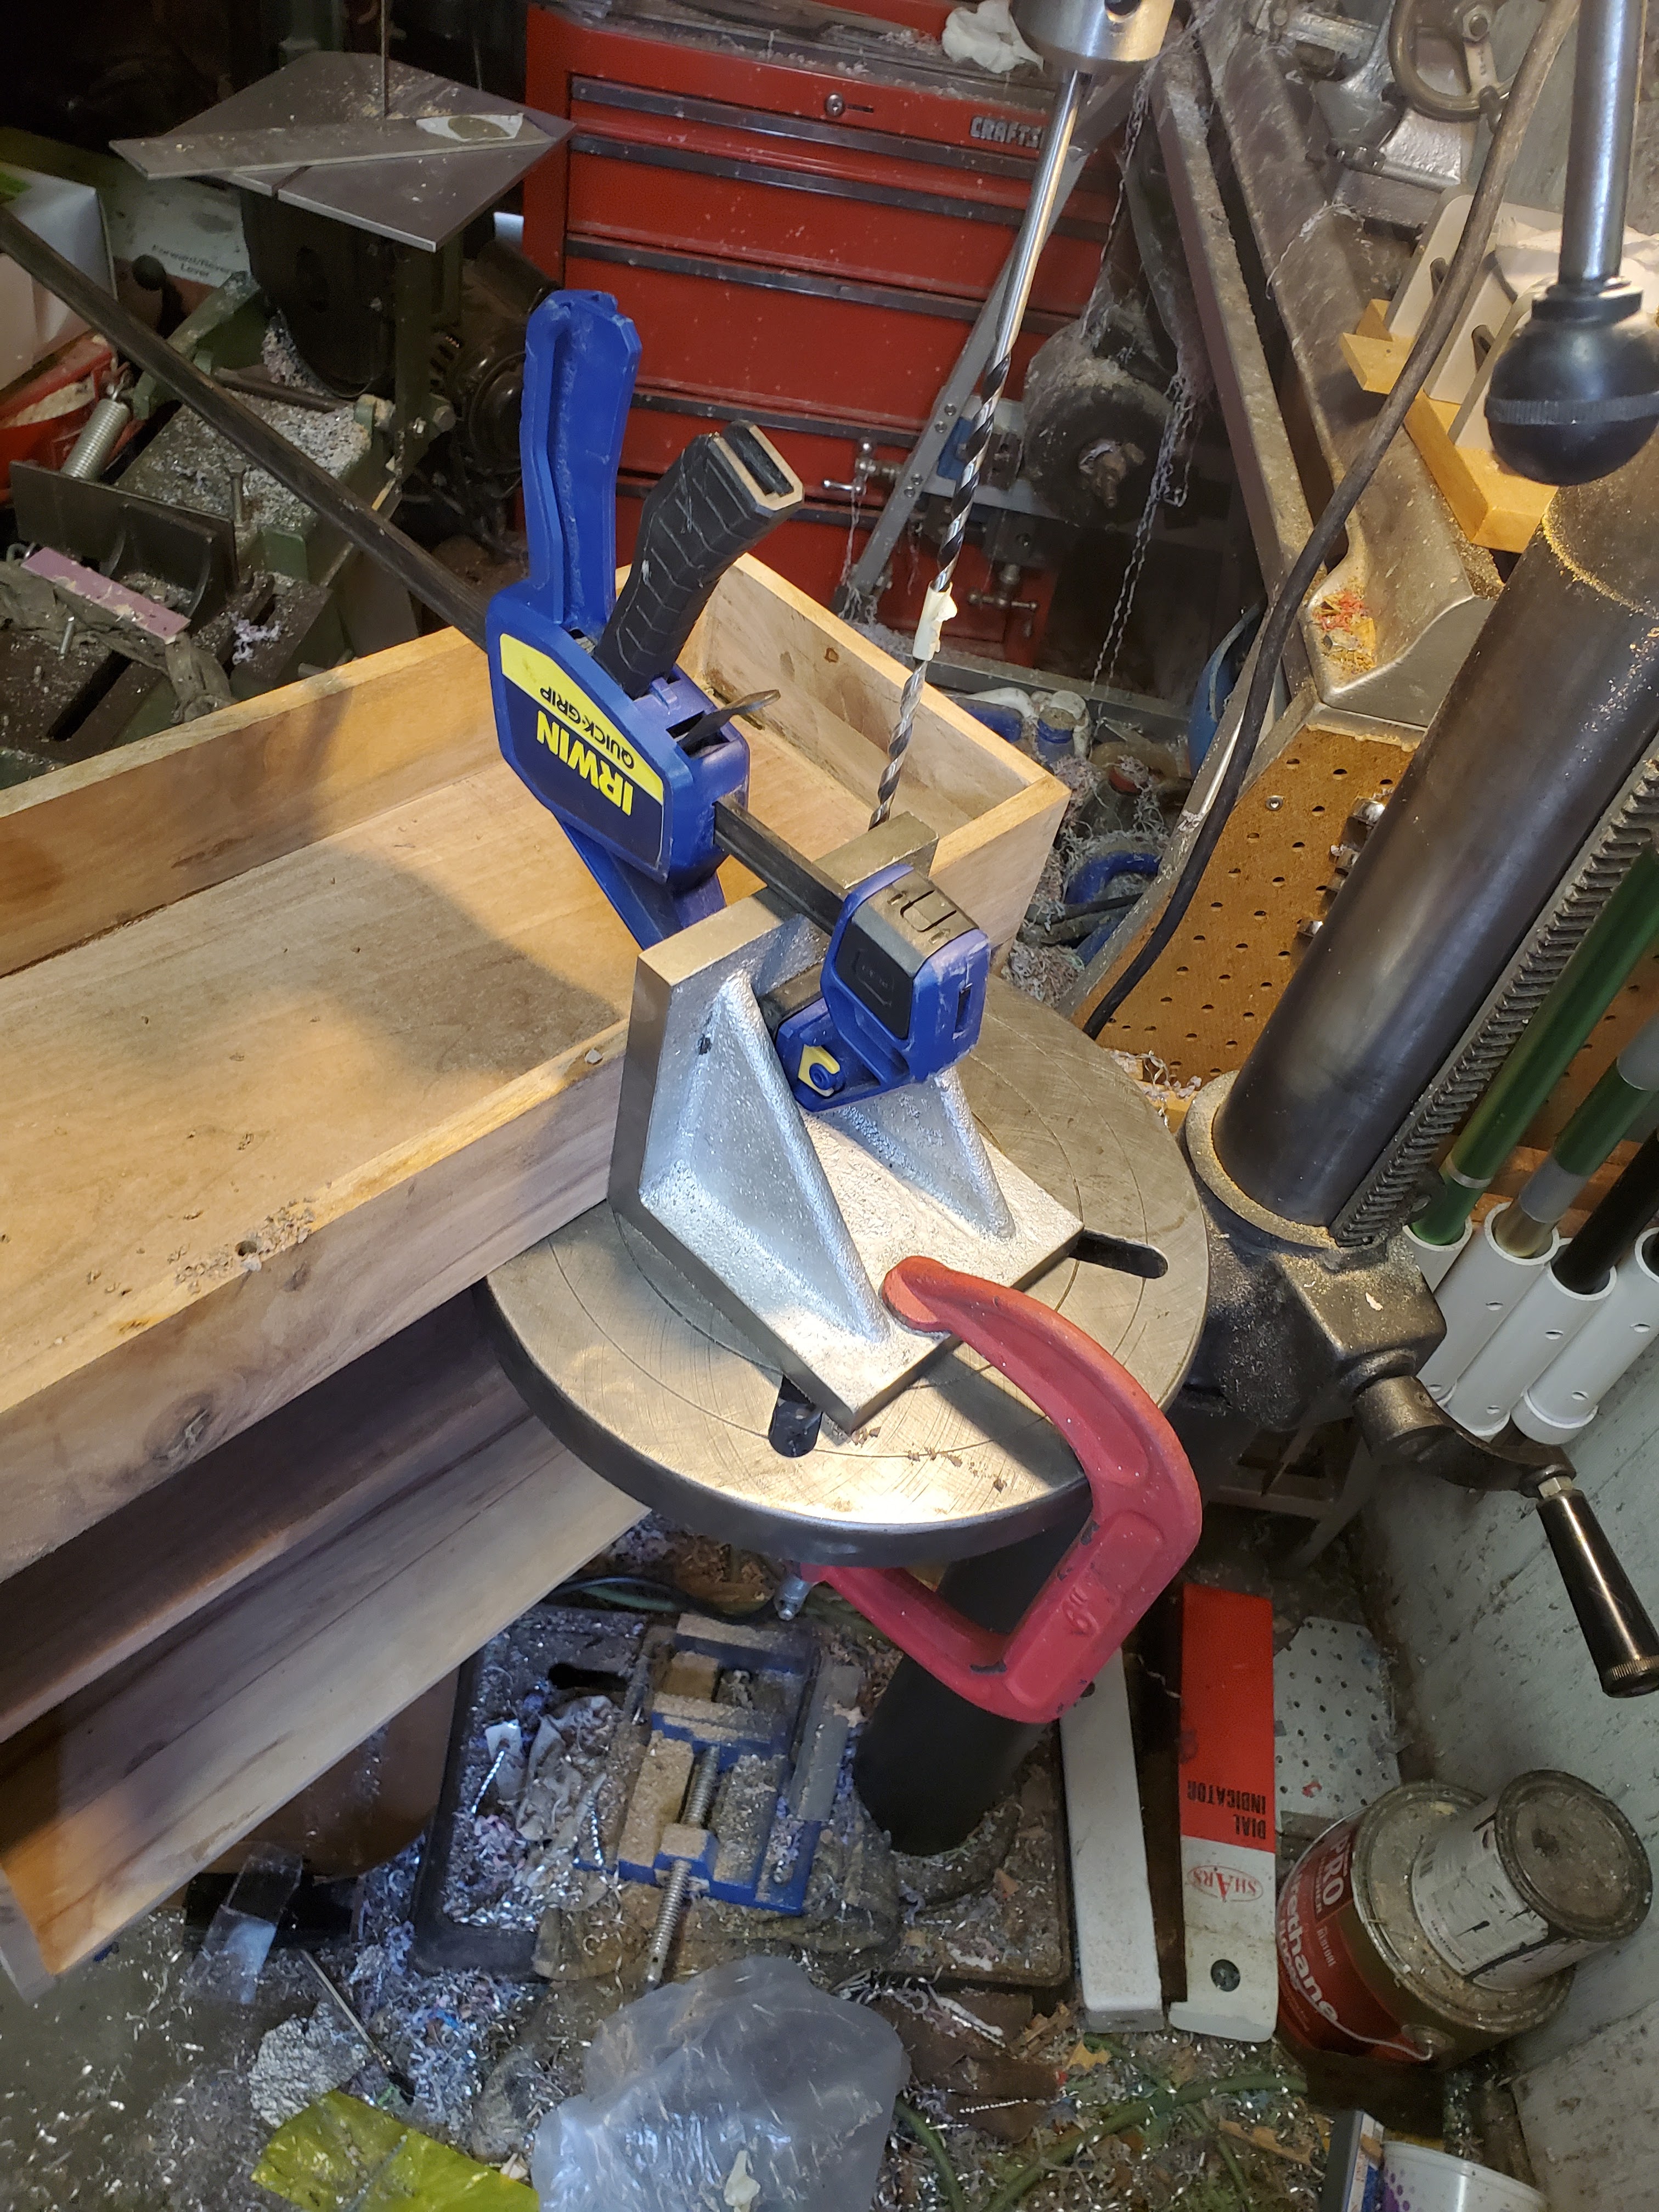
Then, I could finish the drill with a nice, grabby 5/16", 135 degree jobber drill to do a better job of self centering than the brad point bits along that 1/4" bore.  I thought about a drill bit grinder for a 1/4" counter sync, and just decided to wing it.  We'll see in the future if I scrapped all of these in one fell swoop.

After two of the three chests drilled, I was posting over on the machinists forum, and someone pointed out a Craftsman "PortAlign" - an old portable jig used to drill precise holes.  Right there, the lightbulb went off in my head and screamed something about me being an idiot and spending hours on getting things aligned for the drill press, when all I had to do was use a stupid doweling jig!  So, let's do it.


I used a jig that had easily replaceable pins for the hole sizes I needed (1/4" for the through pin bore, and 5/16" for the brass end bushings that keeps the spring and pin in place once installed.  All told, this took me so long in comparison to the drill press method, I was crying (it was 15 minutes for getting the jig set up, drilling the first hole, swapping the bushing, and drilling the second hole to depth, then repeating for the other hole.  A quick flip of the chest to finish the underside 5/16" bore to 0.265" on both of those, and it was done.  15 minutes... is WAY faster than a few hours per each hole working on alignments.

How on earth did I miss that as an option?

The pin drilling is done.  Phew! I had to use the short hand drill for the underside, and as long as I did it okay, I should be good.  Before I can install the inside draw walls, I had to build a new tool.  I went as far as drilling and tapping two ends, 1/4"-28 for a fine thread adjustment (one left-handed thread, the other right) to make a new machinist "jack" that was long enough to make the sides parallel.

I struggled with the right handed thread as the stainless bar became work-hardened in the middle of it.  It still fit what I needed, and I could flip an end around to adjust to a different size.  But it was at this point that I realized that 1/4"-20 (course, not fine) threaded rod and some long nuts would have been sufficient.  So, a quick trip to the big box store (because they had it in stock and I was impatient), and I cut a threaded rod in two pieces and cleaned up the threads on the cut.

With those tools created, I could trim the boards for the inside, and use these crude, long machinist jacks to ensure parallelism of the walls.  First, it was a matter of getting dimensions for the vertical.  This included the entire vertical height, as well as the distance from the bottom (or the top) to the first drawer slide, just so I could make sure they were even.  Making notes :


Then, trim them the last few thousandths of an inch to fit.  Let's glue those in place.


I glued the final strut in place, and let it sit for a day.  The clamps were removed :

I fed them through the router to curve the corners (I should have gotten chrome/nickel corner protectors that were 1/4" radius, but I had mistakenly gotten 1/2" radius).

I did also have to do the final fitment for the front panels, but that went relatively decent.  The process did tell me my table saw sled is 0.8 degrees out of square, so that is an issue for a future fix.  In the mean time, panels have been trimmed.

I spent a few hours sanding to 800-grit (perhaps too fine for lacquer?), and then sprayed the insides of the top bin on both, as well as one side of the front panel.  This was so I could keep it consistent on everything else.  It was three coats on this first phase (30 minutes apart).

 It looks like the gold epoxy actually jumps out once coated.  The darker, "character" walnut seems to pop with the gold.  (Remember, it's not black walnut, this is a combination of sapwood walnut and outer walnut, so it has an extreme grain to it - and it is absolutely gorgeous.)


The silver epoxy, on the other hand, seemed to turn black.


This sat for a weekend, and the following Monday, I shot the final outside coats (three coats at 30 minutes a part).  I let it sit for a day or two, and then I installed the hardware.  This was a make-or-break point - either I was successful up to here, or I could turn this into a junk heap fairly quickly.


Again, the dark and the gold seem to just pop.

This sat for a few days (even though the lacquer was dry in 30 minutes, I just felt like I needed to let it sit a little longer).  Now for the hardware.  First, installing the corner protectors and the hinges.


Next, I needed to get the front panel plungers installed.  These came from Gerstner, since I knew they had a system that worked.  The kit is one half of what you need - e.g. a single plunger, spring, one grommet for the panel, and two brass bushings - I had picked up a few kits when I knew it was for one side only, so two per box.  I glued in the top bushing, let it set up for a few hours, and then glued in the other side.  On one box, I did have to chuck the plunger up into the lathe and trim it down 0.432" because of the size, but they are currently glued up and setting overnight so that I have a solid base to start the latches and handles.


The interesting thing on those plungers is that the lid surface is simply a carpet tack placed in the right spot.  Gerstner did well with what they had - I was thinking I might have to make some brass plates, but finding the tacks in the kits was a good thing.

Next comes the latches and locks.  I debated on installing a key on the brass one.  I'm still undecided, but the latches are all in place.


I must say, these are looking fantastic.  The front panels were simply set in place for the photos.  Before I could call these done, the panels needed to have the hole drilled and the brass grommet installed, as well as the lower hinge hardware for the panel.  I was dreading the panel installation.  It turns out that the installation is documented on youtube by Gerstner.  So, it's off to the drill press to drill the tops, install the hinge plates into the chest, and the hinge pins onto the panels.

First, in go the chest hinge plates so we know how thick to make the panel hinges. Unsurprisingly, it's just appropriately sized tacks that hold it all in place.  Once that is done, install the pins in the bottoms of the front panels that go into those and the panels are the right size (those are drilled out with a #22 drill bit for a tight fit).  I did toss some wood glue in to set up the depth on the pins into the front panel.

The final step is to install the plunger grommets into the top of the panels.  The reason why we do the bottom hinges first is so that we can open the lid, close the panel, and give a slight rap on the pins with a hammer, indenting the top of the front panel with where those go.  Drill them out (I went with an 11/32" diameter brad point bit about 0.040" deep to allow them to be flush with the top, followed by the 7/32" about 0.410" deep).  Then, a little glue to "bed" them into place, pop them in with a light ball peen hammer (the rounded nose allows the grommets to be installed without damaging surrounding finish).

Phew!  It was time for a photo op - these have been a long time coming!


And all three :

Really, this has been a fantastic project.  However, I have learned one thing - if you want a high quality, wooden tool chest, what Gerstner charges for one is well worth it.  The time I have put in (at a standard consultant rate of $70/hour) calculates to about $7,020 (not counting the cost of the hardware or wood, either).  Considering you can get the Gerstner pro-series (the big one) for $2,495 (US), the only thing you get by making your own is being able to say you made it yourself, and Gerstner does sell kits to put together your own that include everything for even less (about $1200 US - I don't know if sanding will be required, or what you'd need to do to complete them).  If you have to go cheap, consider the Harbor Freight "Windsor Designs" chest as it is a fraction of the price.  Sure, it doesn't have the same fine sanding and finish on it, and it's not quite the same size or drawer count, but it will do the job.  In fact, with the push to digital on the Machinery's Handbook, it turns out that Gerstner no longer sells one that can hold a hard copy of the machinist's bible, so the drawer orientation may not even be an issue.

Really, these custom-made chests are keepsakes. They are going to be farmed out to people I know with some specific uses (one was made with more gap between the front panel and the drawers in order to house additional and custom wood panels for what he does, another one is to house some of my fishing tools (rod making, fly tying kinds of things), and the third one is going to someone who has started the dangerous dive into metrology.

Now I have to make 33 customized drawers.  Ugh.

Thursday, December 8, 2022

Puffed Out Chest - Part A

The table project from over the late-summer/fall/early-winter had a few left-over beams.  I decided to try my hand at making a few Gerstner #42 tool chests from some of the boards, in an attempt to flex my woodworking muscles.  This is going to be similar to the table top exercise only in a few parts.  There are eleven panels for this, and I'd suggest a quarter of an inch bigger in every dimension to ensure that when you are done, you have good sizes that can be trimmed back down :

  • Back panel (20" wide x 16" high)
  • 2x side panels (16" high x 9.5" deep)
  • Top and bottom panels (20" wide x 9.5" deep)
  • One front, top panel (20" wide x 5" high) for the top
  • One front, movable panel (not glued into the box) (20" wide, 11" high)
  • One internal bottom for the bottom inside the lid area (19.5" wide x 9" deep)
  • One horizontal, internal drawer separator (19.5" wide x something deep I can't remember)
  • Two vertical drawer separators (can't remember any of these dimensions)

The process is :

  1. Slice the beams into boards (showed how to do that on the table project linked above, and I'm too lazy to show it again)f
  2. Plane the boards down (just over 1/2" for later sanding to final dimensions) (again, too lazy)
  3. Rip the boards to length to give clean edges (lazy... sensing a trend here)
  4. Slice the boards to length for each panel (TL/DR [too long, didn't read])
  5. Cut dowel or biscuit joints/holes into the boards
  6. Glue them up
  7. Apply epoxy resin to fill the nail holes (and other imperfections)
  8. Trim the boards to both squareness and size
  9. Cut box joints (a new tool should show up here to cut these)
  10. Use a router guide (another new tool) to cut the slots for the draw runners)
  11. Drill holes and cut mortises for panel locks, hinges, handles and actual key-locks
  12. Test fit everything together
  13. Final sand all of the panels to prepare for the final glue up
  14. Glue everything together
  15. Stain (if that is going to happen)
  16. Coat with a varnish or other protective layer
  17. Install the hardware
  18. Make a lot of drawers

Oh, yeah... I'm making three of them (for a few people).  (WHY do I always bite off more than I can chew?)

So, with that let's get moving.  I have a feeling (with how long the table top exercise went) that this could be a long project.

I sliced the beams down to length, planed them to thickness, and then ripped them lengthwise to get my basic building blocks.


Next, I sliced them all to length for the panels I needed.  Here are two tool boxes organized in "panels" that aren't glued up.

Okay.  The next phase was something new.  I had a biscuit joiner, but my weird little brain said this was a good chance to try my doweling jig.  I took the panels, and I'd drill a hole in the side using the jig to get perpendicular.  Then, I'd use the little nub that the jig came with to transfer the drill hole to the next board, and then (using another scrap board in between the hammer and the board I'm marking) I'd give a slight tap to transfer the point to the other board.  Then I could use the same jig to drill new holes in the mating board.  So, here we go.  First, drilling the board :


Then, marking the next board :


At this point, I can glue the panels up.  Lots of clamps would have made this MUCH faster, but I could only do one at a time.

I never did the holes in the same places.  I had this fear that I'd mix up boards and get grains all wrong, so I intentionally placed the holes at different points along the boards.  I put two dowels in the side panels, and three along the lengths of the front, folding panel and the top, bottoms, and the back.  That should give some strength instead of a simple butt joint, and make this chest fairly stout and solid. I am doing 1/4" dowels for these, as I'm working in 1/2" wood.

It was at this time I wore my hands out (drilling and transferring holes and drilling the other side for 156 dowel, but who's counting?), and tried biscuit joining them - but that had horrific results.  Those panels became the internal panels, because they could be cut a little shorter.

With the panels glued up, and with me organizing as much color grain continuity as I could, I had one tool chest with slightly darker walnut (transition from sap wood to heart wood) and two tool chests with the lighter wood (these are walnut, but not black walnut).  With the slightly-darker walnut, I'm opting for brass hardware (which means a gold epoxy), and the other two will be chrome or nickel hardware (which means a silver epoxy).  I went with "queens gold metallic mica" by Littarby to be exact, and I went with the brightest silver I could find (just "silver").


The filling process also took as long as the glue up - I didn't have enough work surfaces, and I could only do one surface of each panel at a time (there are 6 for each panel - both faces and four edges - but I always left one edge along the grain exposed for a base surface to use when trimming to size later).


This, alone, was about a month in labor, continually mixing up epoxy, vacuuming the bubbles out, and pouring it over every single void (or crack where the edge wasn't lined up perfectly when ripping to length), and repeating for the same surface until the cracks and voids were full.  I'm not using a fast cure on epoxy, primarily because I want to give it time to slowly get into the cracks - essentially, I want every void in these boards filled with epoxy.

On edges where a crack transitioned to, those also mandated a surface for pouring (and there were a few).  All cracks on the edges were filled, and most of the end-grain was also filled as much as I could get.  I did this by taping the ends, standing the boards up, and pouring into the tape "moulds".

Once the epoxies had cured, I could finally get to the sanding.  This was a bit annoying - because I already sanded previously (after gluing) so that I could find the voids.  But, I have to do it again.  I'll do the finish sanding after the routing for the drawer guides/runners.

Unfortunately, there was a snafu in which one of the boards was epoxied to the clamping boards, and releasing it snapped and cracked one of the side panels (not along the glue line, either - that joint seems to be holding well enough).  You can see the crack in the above photo.  This was epoxied together to get a good fix.  At one point, I also broke one of the sides - this was glued together (with a biscuit to give the joint as much strength as I could).

 There was so much sanding to be done that I ultimately used a grinder to knock large swaths of epoxy down to "close enough" before engaging the sander.


You can see in the pictures above that I have three piles of boards on my workbench.  Each pile is a matched set of panels.

 It was a lot of sanding the epoxy used to fill cracks down, but the day that happened was a BIG day!

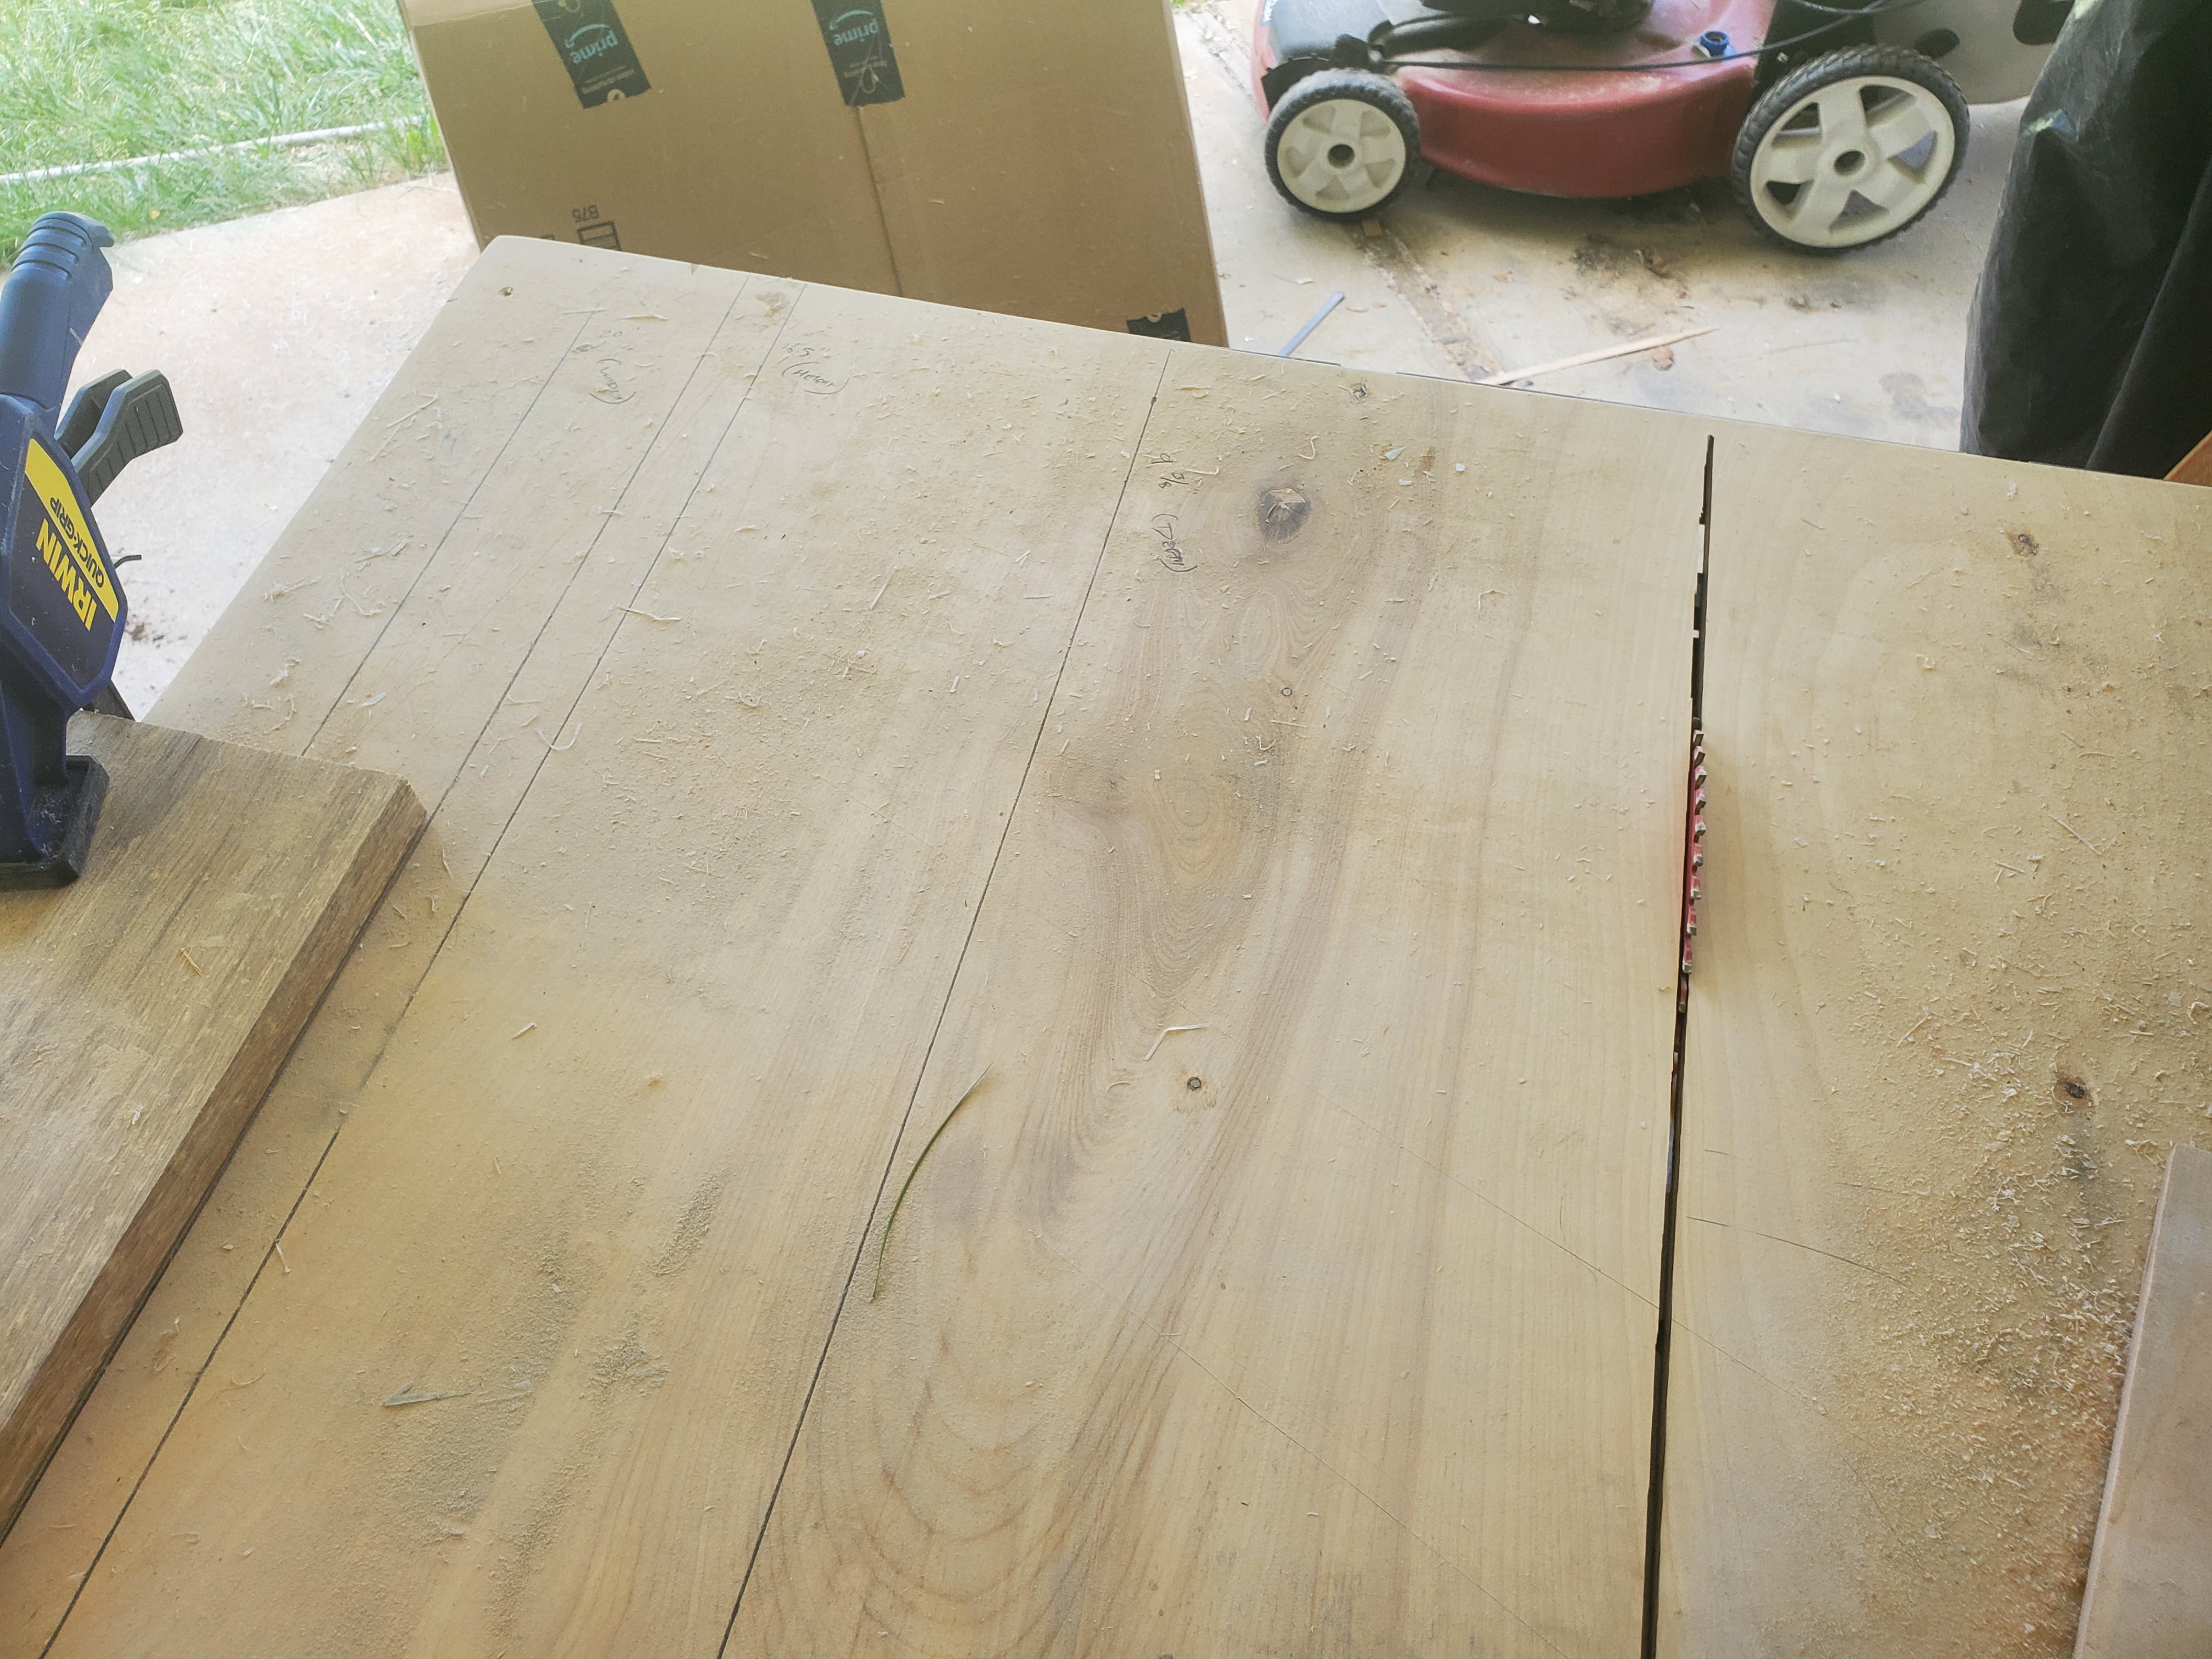
Once the sides were sanded, the boards could be cut to final dimensions on the table saw.  Each board had a single, good edge at this point.  I'd first cut the parallel lengths for each board with that length, then I would move on to another dimension and cut all boards for that one (on all panels).  As each cut was made, a mark was put on it to know which ones were done.  The marks were in pencil so that they could be sanded off once the box was glued together.


If you look closely at the last picture above, you can see I put marks for widths of each panel on my panel sled.  It's a technique called "story boarding" - you write down exactly what will happen, and then you make it happen.  I would set one width, mark it, put the stop block clamped down, and then make ALL of the cuts that were the same dimension.  In other words, every single width was cut.  Then every single depth was cut.  Then every single height was cut.

The result was a set of panels that were perfect in every way except for... the depth.

[sigh.]

The depth, because of the narrowness of the dimension (supposed to be 9.375" or 9 3/8"), I chose to use the fence instead of my marked story board sled.  Unfortunately, I measured to the same side of the 9" mark, which actually turned out to be 8 3/8".  That meant each of these boxes is going to end up 1" shallower than what they were patterned after.  Oh, well.

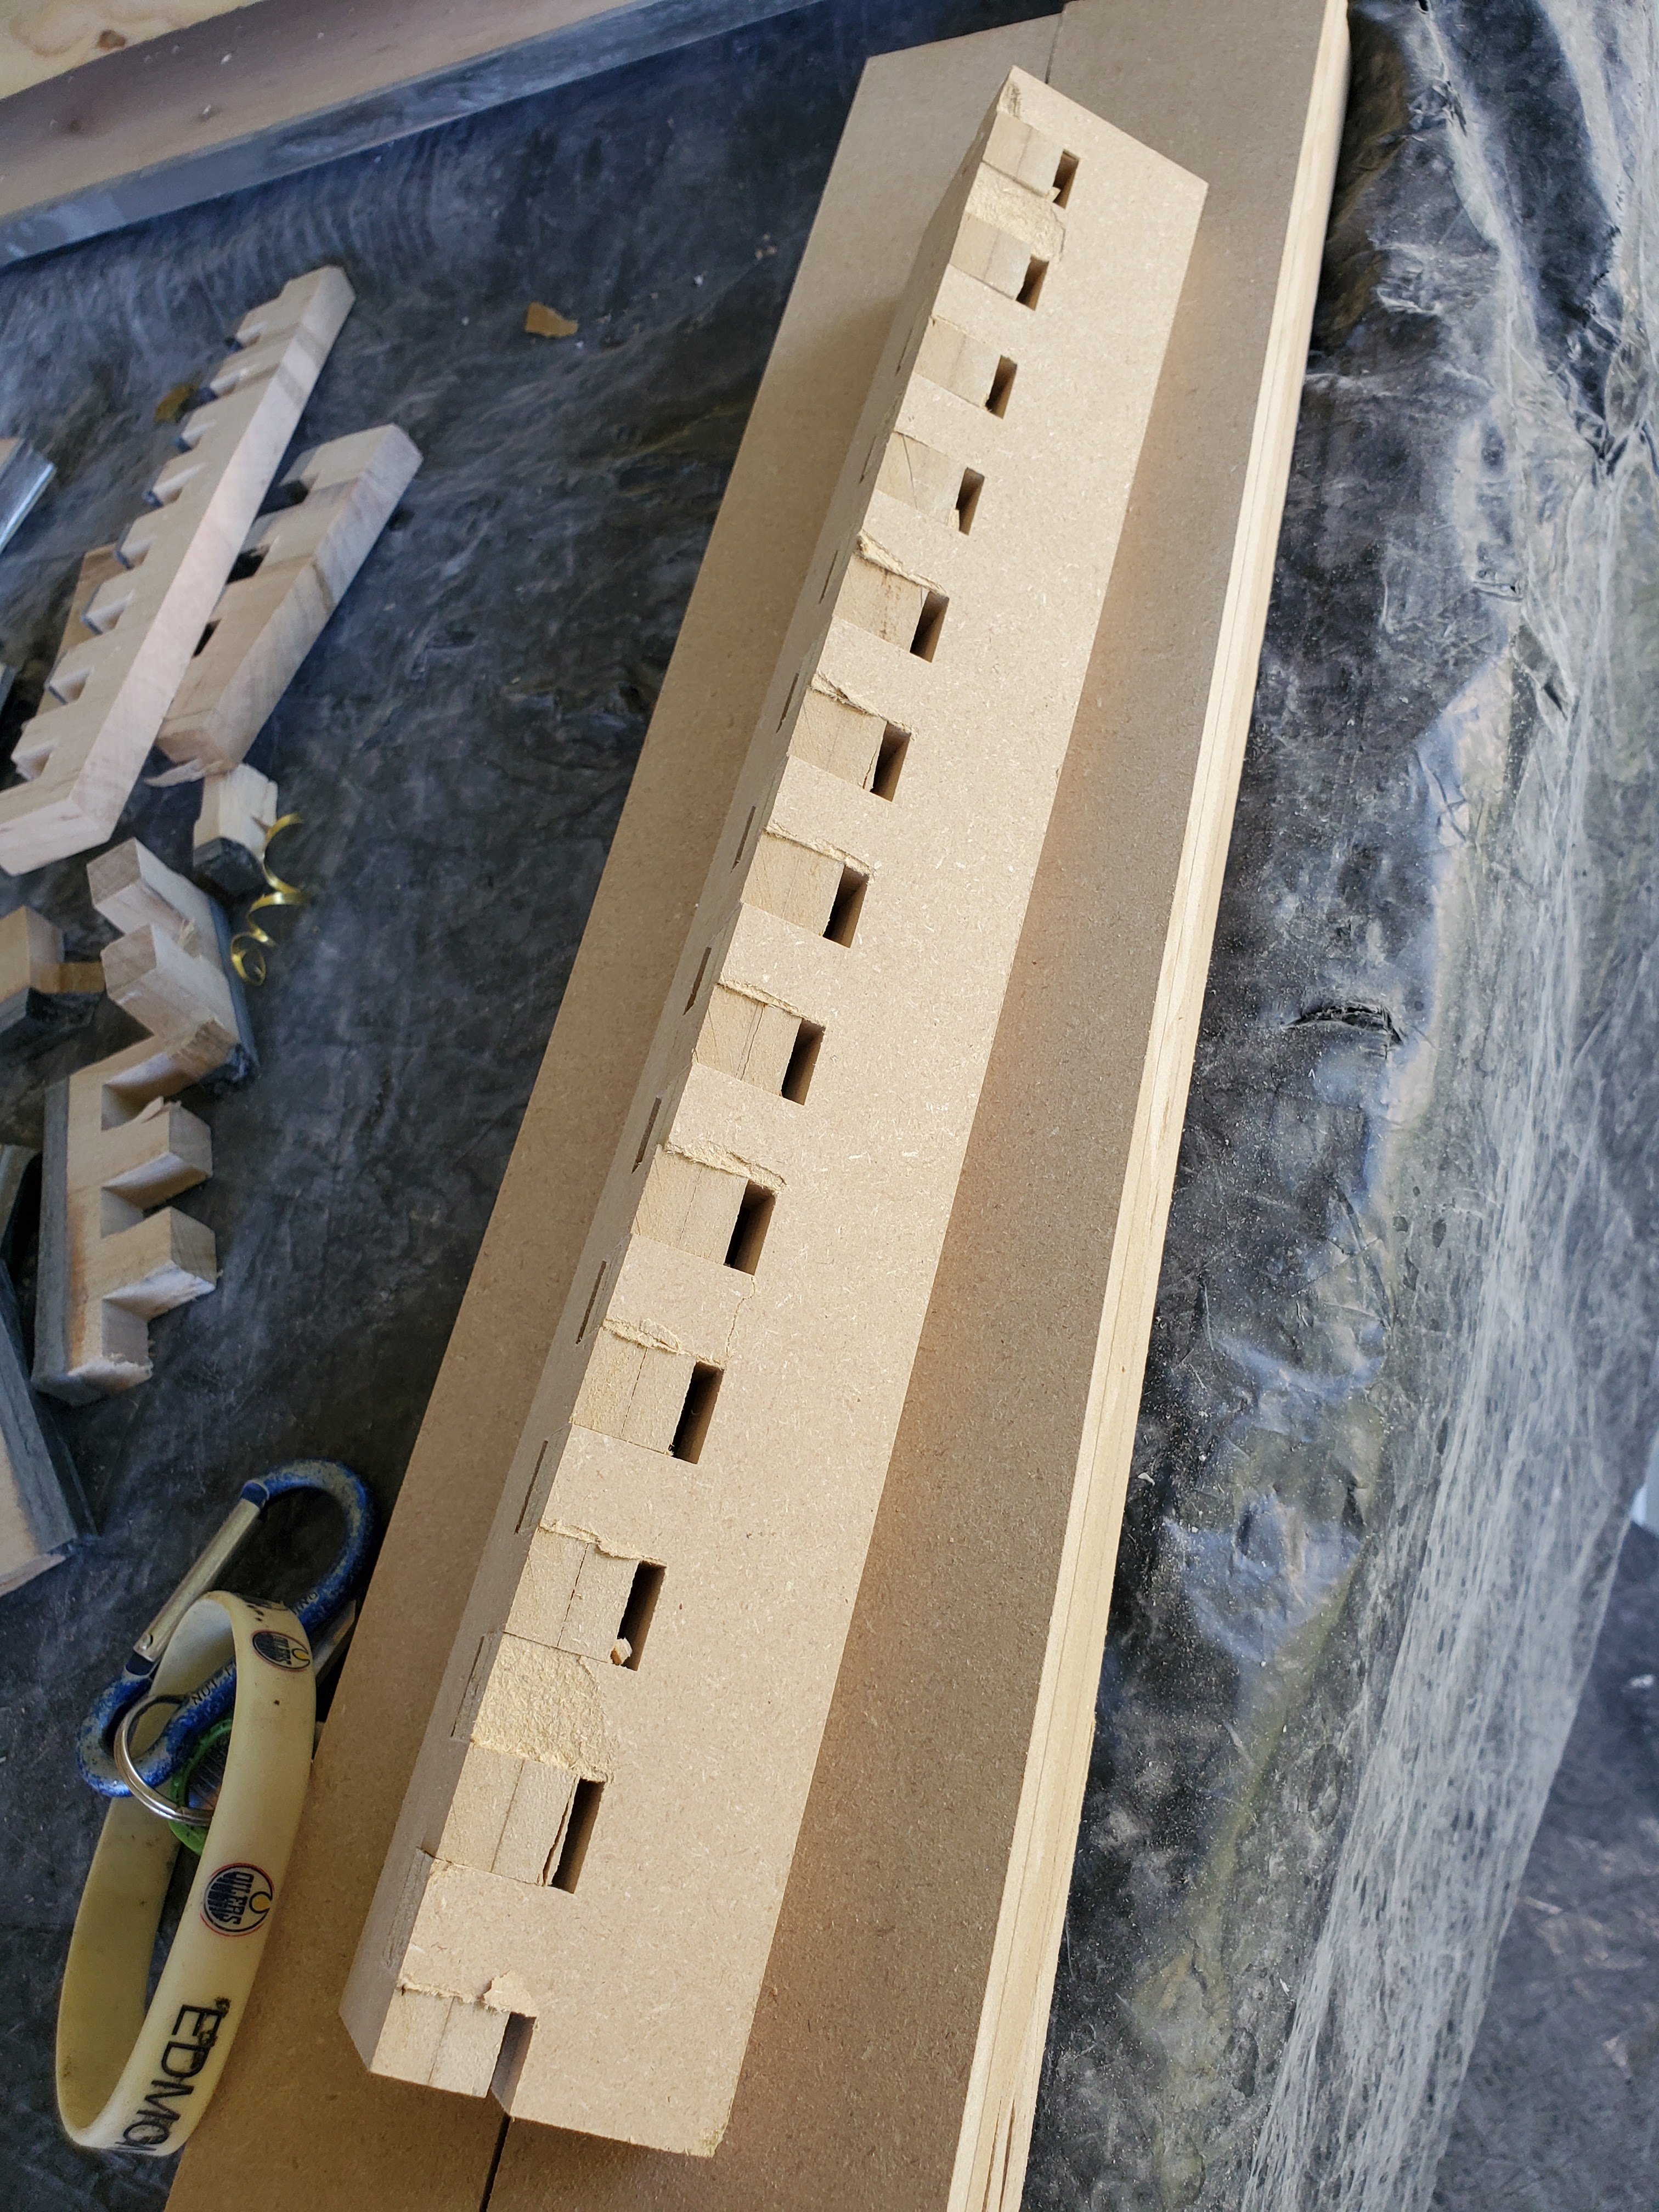
With the panels all cut to size and prepped, I could then cut the box joints.  I had picked up a Rockler jig for cutting box joints on a router table, and before fully engaging, I had to finish the jig.  It requires one pass with the cutter you want.


At this point, I needed to do some careful planning.  I didn't want to mess these up.  So, I had to use some left-over MDF (it was 1/4" thick, but I'm testing for 1/2" thick - gonna have to glue some boards up) to cut some test cases just to see.  I have a couple of oiler cans that I've been collecting, so I decided to use this MDF as a shelf when done.  I've intentionally cut the depth a little too deep, so that I have a slight forked lip all the way around the shelf to keep the oil cans on the shelf when we have another earthquake roll through.

The part that I was most worried about was the corners where three panels met together - and this little test candidate was perfect for the test.  First, glue two "boards" together to get the 1/4" to 1/2" thick (matching the tool box panels).

Each of those boards were fed through the table saw to get them square and to size.  I had three boards the exact same dimensions.  One would become the "back" (toward the bottom, used to attach the shelf) for attachment to the french cleat, one would be split into sides, and the last would be the actual shelf.

It's time to cut the box joints.  It took a while to get the jig set up, because it kept changing on me, and wouldn't line up.  (Widths kept growing.)  It resulted in a lot of scrap tests completely failing.


So, I punted.  I found the device kept sliding, and the dimensions would change with each cut, too.  I grabbed some brass shim stock, and slapped it into the grooves that the jig attached to.

The shims allowed the jig to stay in place long enough to cut a longer edge on both sides.  It was still tight, but it worked.


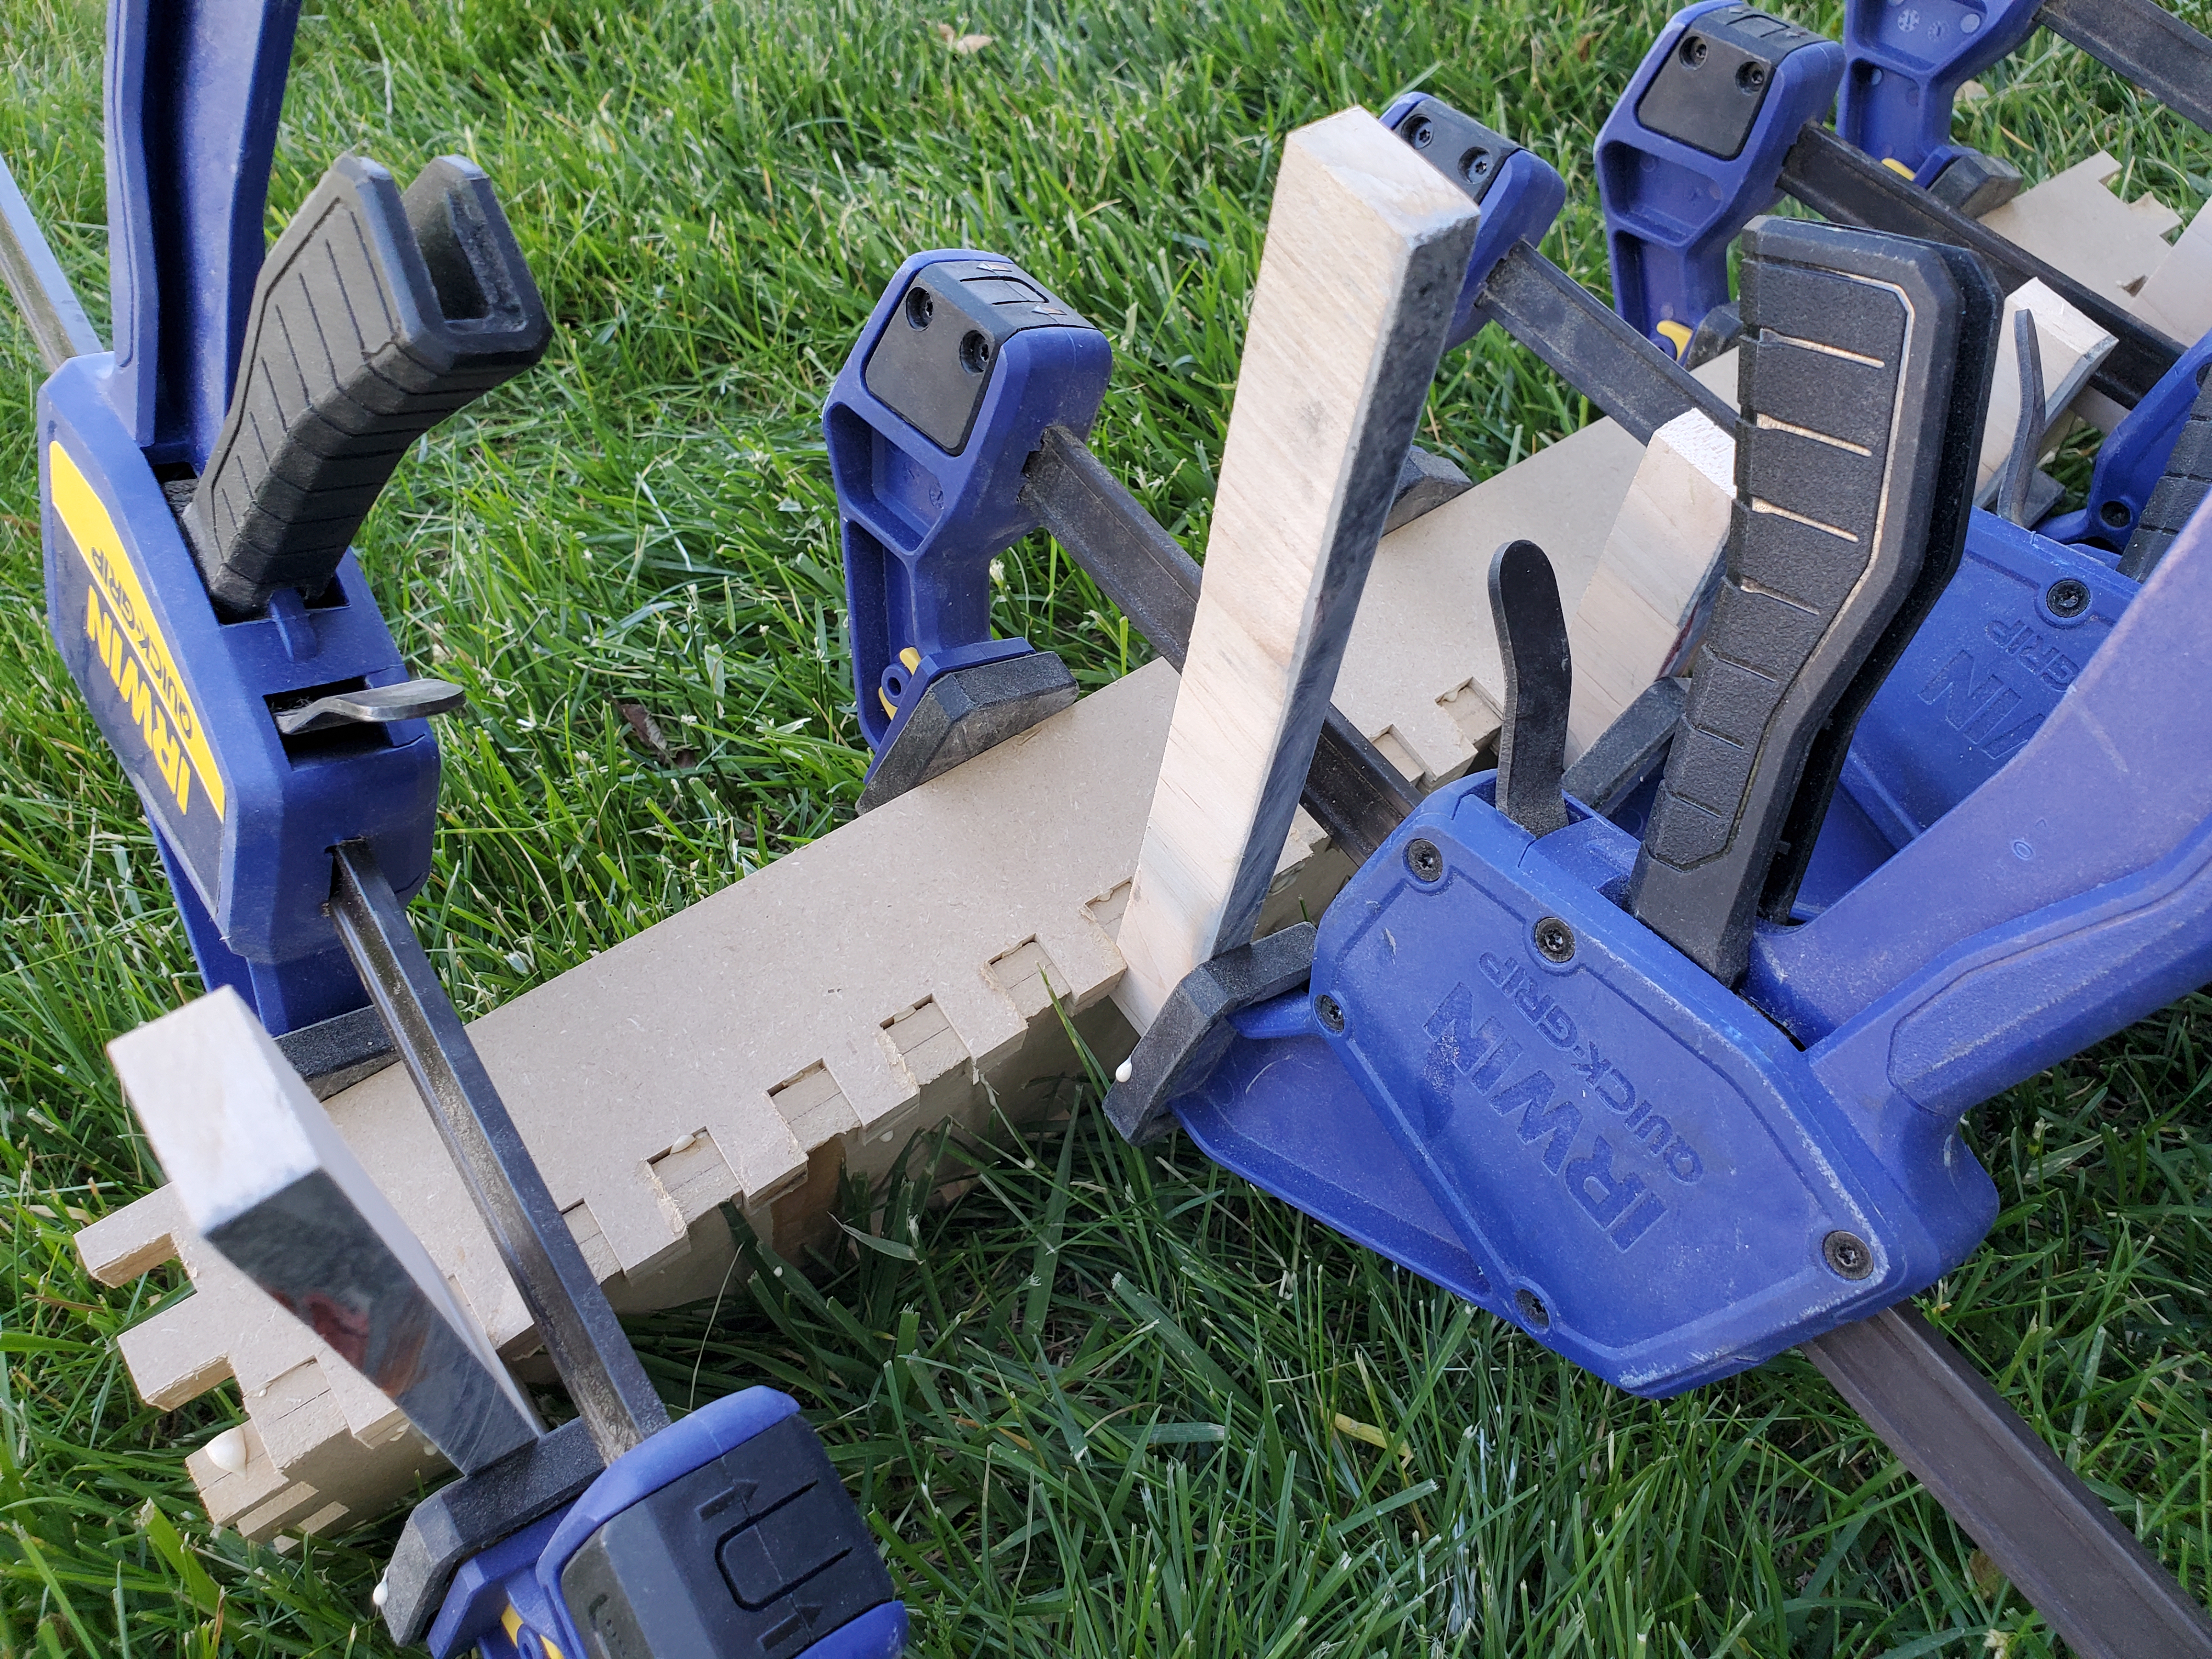
Next up, I have to get back to my test case - the oiler shelf out of MDF.  I ran 4 edges of 24" long edges through the jig.  I also grabbed the side edges (both sides), and then glued it together.


If you look closely, you'll see a gap on one end.  I completely put one single board in the wrong way.  [sigh].  Assembly will be critical.

The other thing that I learned (which is why I did the test) is that, on a box-cut corner where three sides come to a point, the actual corner is not complete - there is a small chunk of wood that is not in place.  It's a side effect of box cutting, really, if you think about it - three sides, binary on/off.  Anyway, I can fill the corners with epoxy before rounding everything off, so I think I'm going to be fine.

Now I can engage the REAL box cuts, knowing that I have to reset the jig after every long edge.  Lots of box joint cutting, each mating surface at it's own time (e.g. cut one edge of a board, then cut the same edge on the adjoining board).  In this way, the joints should be going to be perfectly aligned.  I went through each set of boards and marked every single edge.


I now have three piles of boards, one for each chest.  Now, on to the inner routing that needs to happen.  I have to cut grooves for two horizontal (bottom of the lid, and the separator for the drawers).  This will need to be the thickness of the boards.  Before I could do anything, I ran a test.  I anchored the aluminum angle that I'd be using as a guide, and ran the router.  I could measure the distance from the angle to determine how far I needed to get the cut where it should go.  I needed 2 3/32" with a 1/2" router bit.


Okay, now I can cut the shelf support grooves.


I only hosed up one tool box and got a groove on the other side.  Yay!  I'll just fill that apprentice mark with some epoxy, and everyone that sees it will be completely the wiser (too easy to know what happened - it's on the outside).

The next groove I needed to cut was the bottom one for the front panel to slide in.  This was a bit difficult as it was 0.397" from the bottom board, and 0.197" in diameter.  I don't have anything in that diameter - even a 3/16" router bit comes in at 0.1875".  I settled for the 3/32" router bit I picked up explicitly for the drawer runner slots (more on that later), and then did a lot of math until I had the right numbers.  Then I could set up a piece of angle and cut the path.  It would require three passes with the 3/32" bit (3/32" is slightly less than half of the 0.197").

While there, I routed out the metal frame so I could inset that.  Gerstner sells the little front panel pivot point that keeps the wood from splitting out when people abuse it.  I'll need to order two more of those (for the other two chests).

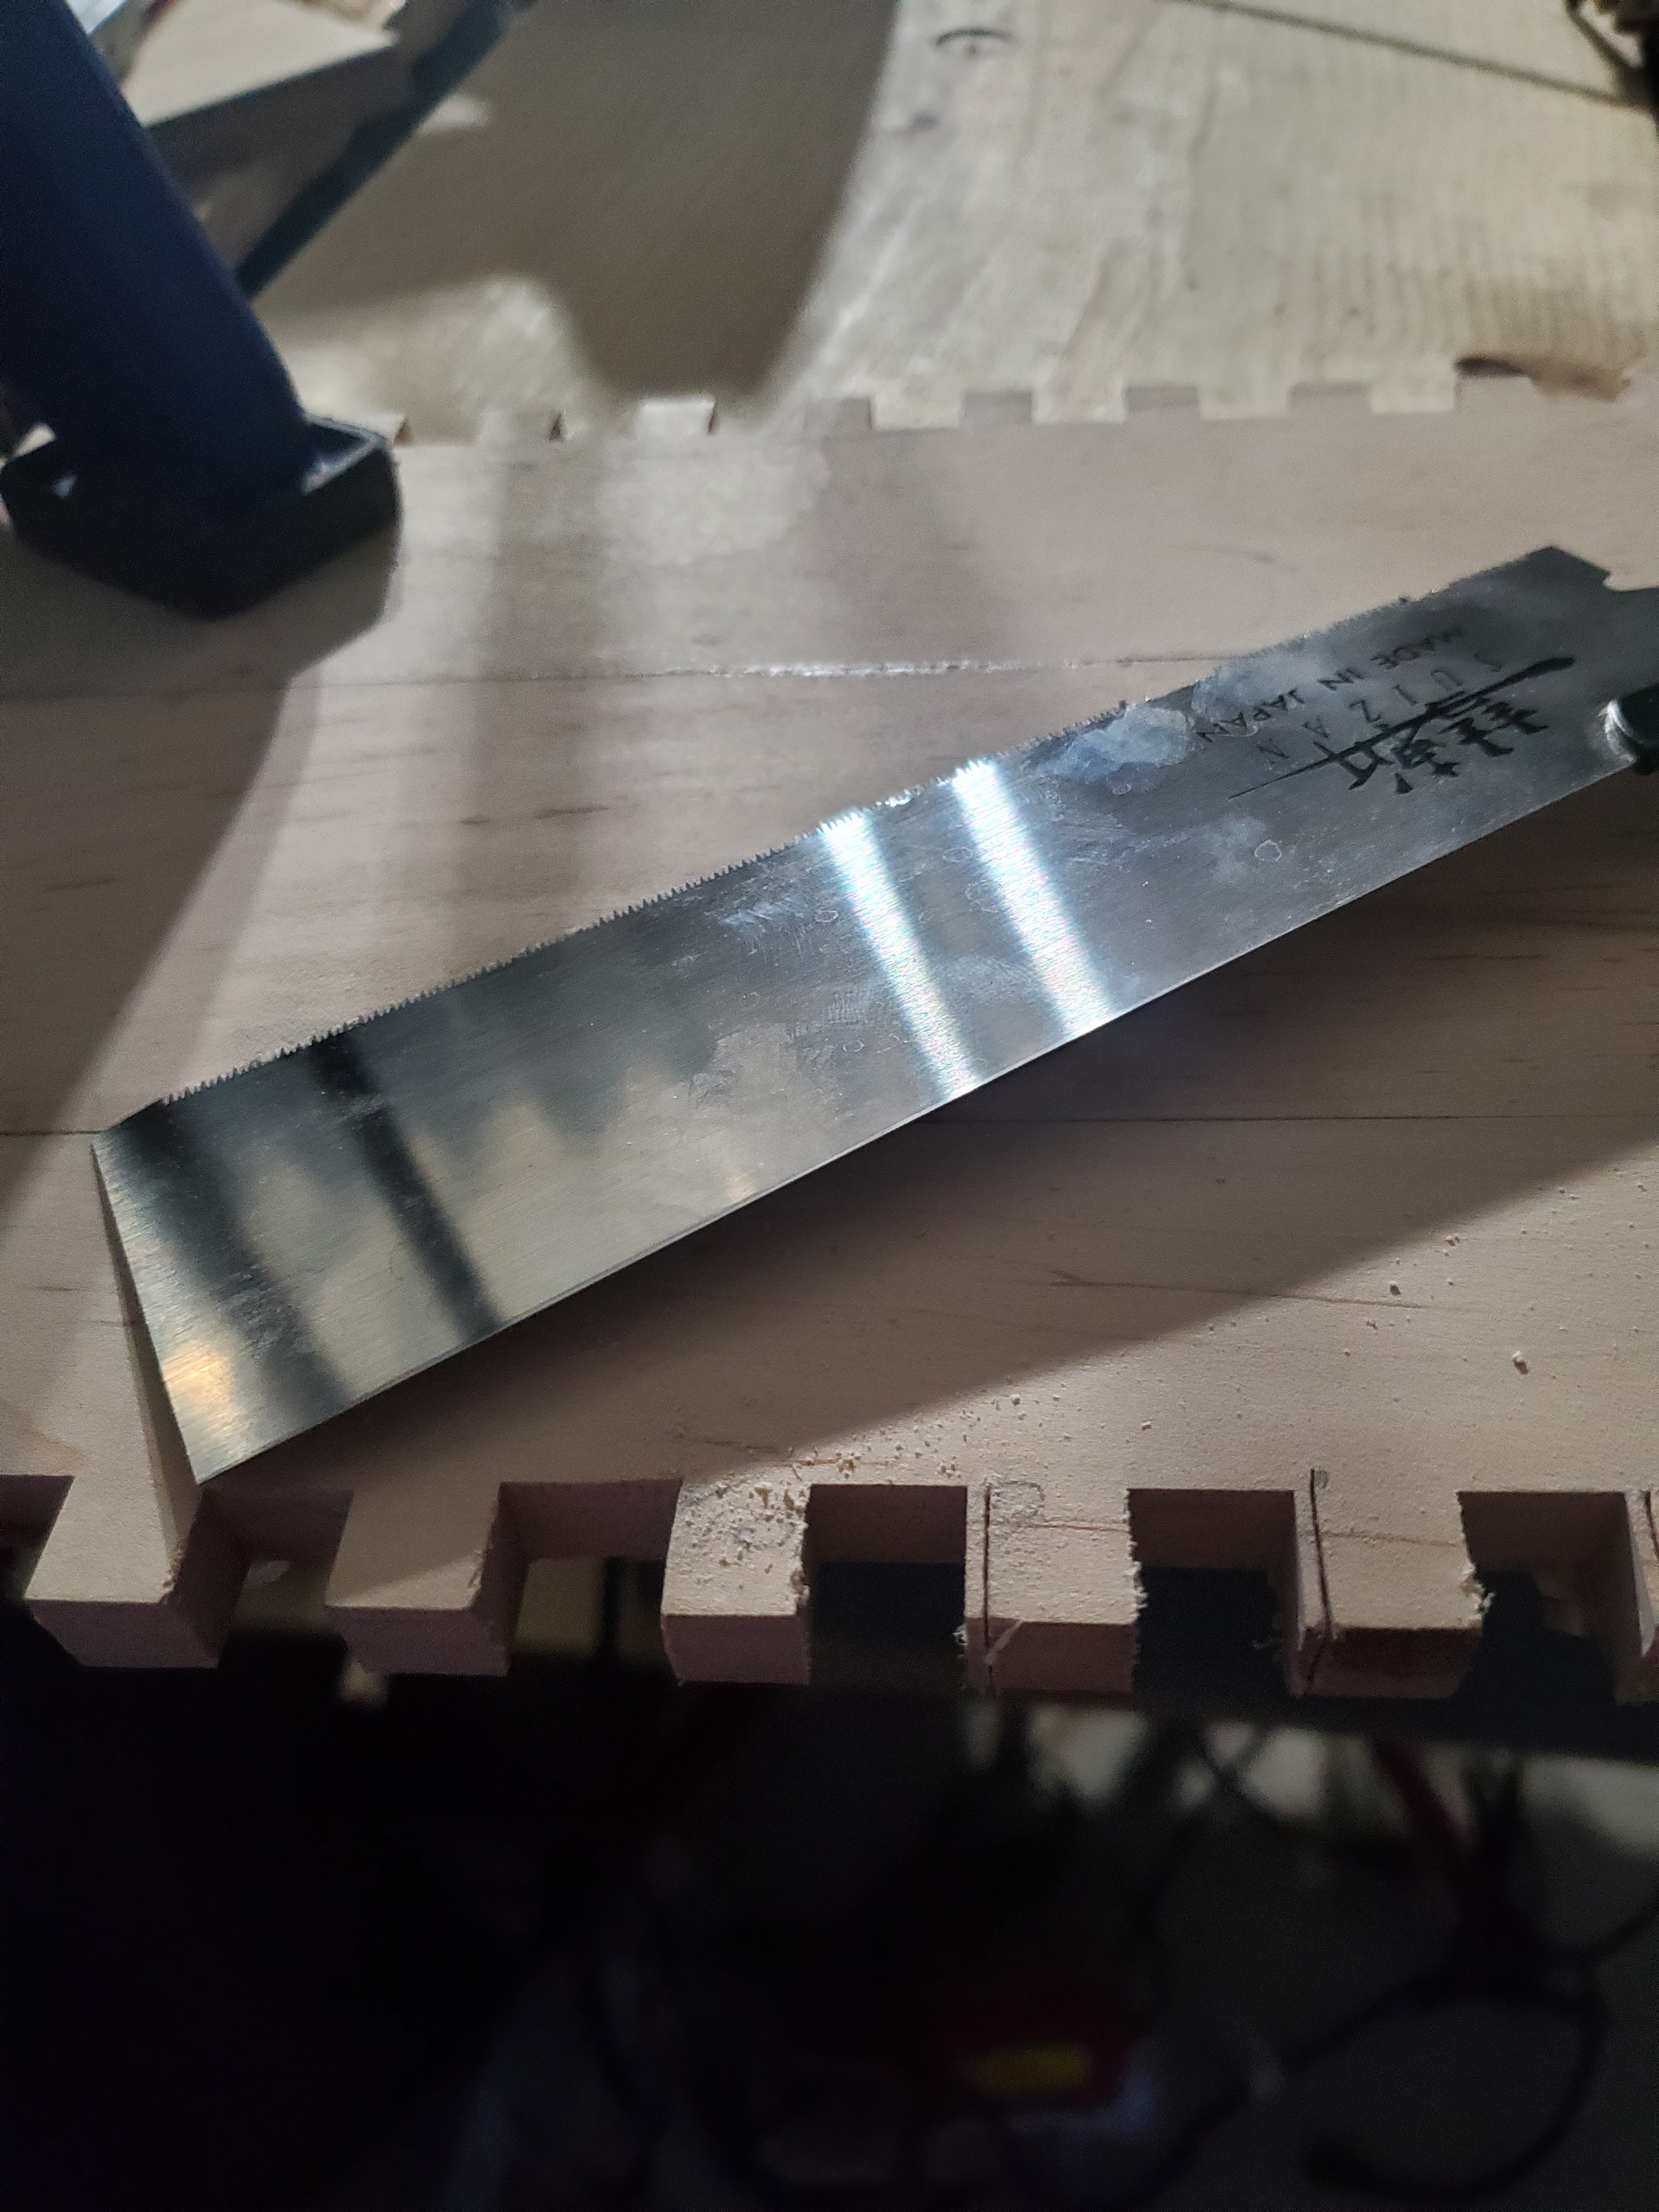
Unfortunately, the box joints didn't quite line up perfectly.  I had to manually fit each joint by hand using a rasp, a Japanese pull saw, and sandpaper glued to a 1/8" metal bar that fit between the pins.  I gotta tell you, for joinery, those pull saws are amazing.  I'd set the edges together that were to be joined, and transfer lines from one to the other board just using a pencil on the edge.  The pull saws could make some very thin slices, and things just came together quickly.


Three boxes' worth of hand sawing various tenons for these box joints was excruciatingly time consuming.  The rasp, hand sand bar that fit in between the tenons, and the pull saw/coping saw combination did the job, but it takes a while to line everything up.  When the day came that these were done, I was ecstatic. I still wasn't remotely complete.

My next task could only be done assembled without being glued.  I needed the actual inside dimensions of those grooves I'd cut.  Sure, I can measure where things go, but with the difficulty of things potentially not lining up, I am going to make absolutely sure.  So, I put the boxes together and slapped some measuring "bars" in place.


Granted, because I don't trust the tape measure on the inside of a tool box where I need to measure the groove, so I used a 1/4" piece of MDF.  Then I could measure the gap using the telescoping snap gauges (yes, a machinists' tool rears it's ugly head).  Each box has to be assembled and checked for this dimension so I can cut the drawer supports.

With these measurements, I could now cut the bottom board for the top area, as well as the drawer supports.  First was the top, because it is very simple.  It's just a rectangular board.  The horizontal drawer frame was easy to, but it needed a rabbet.  And, once the rabbet was cut, I could then cut the two vertical drawer supports to match.  But, alas!  There not enough wood here to finish the supports for the drawers!


The next task was routing the grooves for the drawer runners.  This task turned out to be a lot of math.  First, I had to determine the distance from the router flat surface to where the router bit actually cut.  Then, I had to calculate for each box where to set up the jig (e.g. distance from the top or bottom), and then route each one.  I had to use my wood working machinist square because it had 16" of room for me to play with.


With them routed, I have three piles of chest carcass.

The next step was to sand all the inside surfaces (because I wasn't going to be able to sand them once glued up).  I went to 320 grit, using the old carpenters trick of using a pencil on the surface of each run and sanding until the pencil marks are gone.  Once that was sanded, it was time to glue things together.


I messed up on one side, and had to use one of those fancy orbital saw thingies.  With a 3/8" blade, it cut a 1/2" slot, which matched up perfectly to the 1/2" box joints.  Unfortunately, after that, I was using a chisel, and (while intentionally trying to keep my wrist out of the way), slipped.  An involuntary reaction jerked my wrist right into the path of a sharp chisel.

The doctor was kind enough to tell me how to remove the stitches on my own (which I did - I didn't want to see anyone).  So, on to finishing the glue ups of the tool boxes.


The next step was to cut the tops off.


Now, I should be able to fill the box joint imperfections with epoxy to match (one box in gold, two of them in silver).  I also used a laser engraver to throw my makers' mark on the front panel (inside) on each one.  You can see it in one of the photos above.  I'll use a wire brush to clear out charcoal, and then fill it with epoxy resin to match the rest of it.  Then I can do the final sanding and the hardware installations.  (I did mark the plunger dimensions on each one.)

However, this post is getting very long, so I think I'm going to split this into two posts.  See ya on the next post!